Tower Dryers
Kerone brings over 50 years of experience in designing high-performance tower dryers for a wide range of industrial and commercial applications.
Engineered precision for Tower Dryers.
Kerone brings over 50 years of experience in designing high-performance tower dryers for a wide range of industrial and commercial applications. Built with advanced heat transfer mechanisms and automated controls, Kerone’s tower dryers are engineered to deliver optimal drying performance while maintaining product integrity.
Tower Dryers provide fast, efficient drying for large farm operations and commercial purposes. The tower dryer design utilizes industry proven drying principles along with many unique features to provide the commercial user with a simple, reliable, fuel efficient grain dryer.
Our advanced AI, ML, and IoT technologies, this solution delivers smarter automation, real-time insights, and predictive intelligence to enhance efficiency and drive future-ready growth.
Continuous tracking of process parameters with instant adjustments.
Intelligent fault detection to prevent failures before they occur.
The thermodynamic architecture of our Tower Dryers incorporates advanced thermal modeling and computational fluid dynamics (CFD) to ensure optimal heat and mass transfer across the entire processing zone. By precisely controlling thermal gradients, air velocity profiles, and direct energy delivery mechanisms, the system achieves uniform treatment while preventing localized overheating, product degradation, or thermal stress. This balance of intensive heat transfer and controlled retention time ensures maximum operational throughput with minimal specific energy consumption.
Built with heavy-duty structural engineering and sanitary metallurgy, each unit is manufactured to withstand continuous 24/7 industrial operating conditions. Contact surfaces are finished in high-grade stainless steel (SS 304, SS 316L, or corrosion-resistant alloys) with sanitary mirror-polish options, CIP/SIP washdown provisions, and hermetic chamber sealing. This guarantees full compliance with stringent international hygiene, CE machinery directives, and cGMP standards across food, pharmaceutical, specialty chemical, and heavy manufacturing applications.
Proprietary control algorithms ensure strict process repeatability, while built-in safety interlocks and electromagnetic shielding comply with international CE and OSHA standards. Full process development support — including material loss tangent testing, moisture sorption isotherms, and pilot trials at our Ambernath R&D facility — ensures the selected technology matches your exact industrial throughput goals.
Product & Systems Gallery
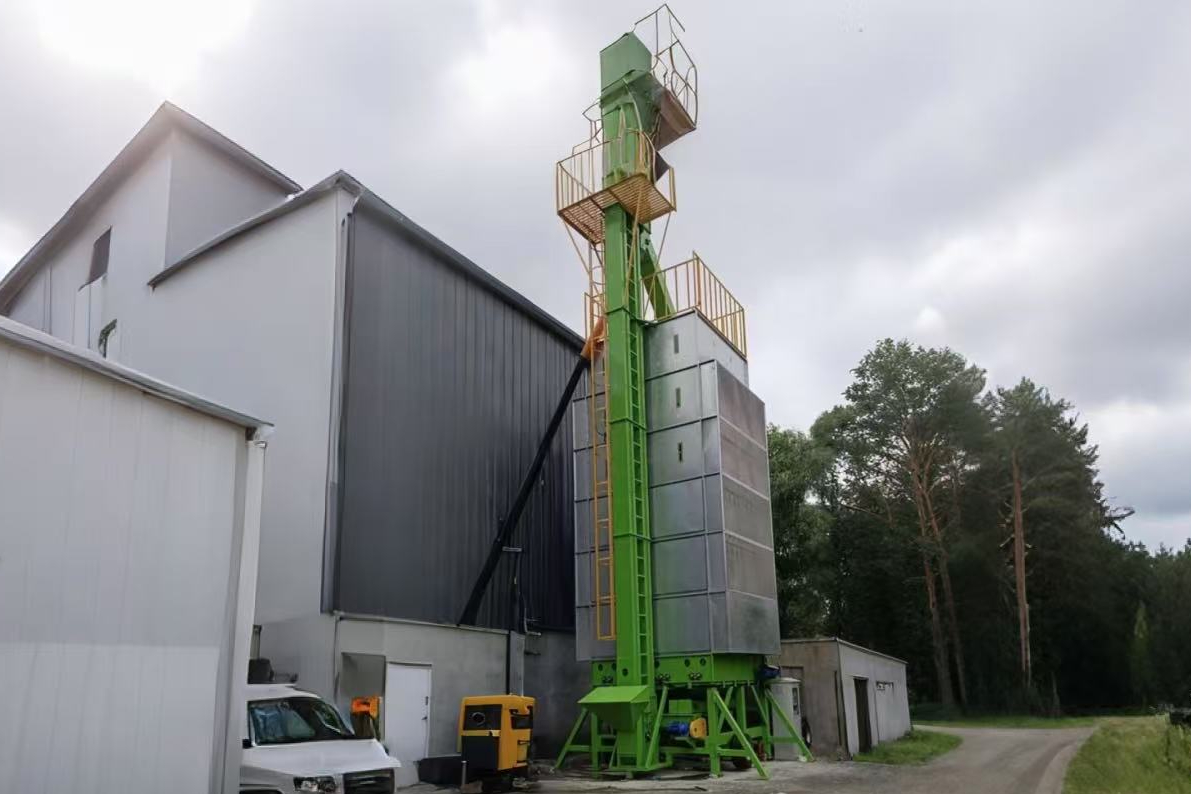
Explore authentic high-resolution photographs of industrial machinery, pilot trial rigs, and continuous turnkey processing installations engineered by Kerone Engineering Solutions for Tower Dryers. Each system is fabricated at our ISO 9001:2015 certified manufacturing facilities with precision laser cutting, robotic welding, and stringent Factory Acceptance Testing (FAT).
Tower Dryers
Click to view high-res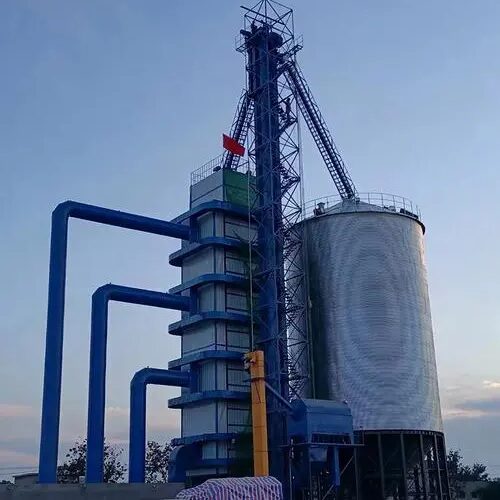
Tower Dryers
Click to view high-res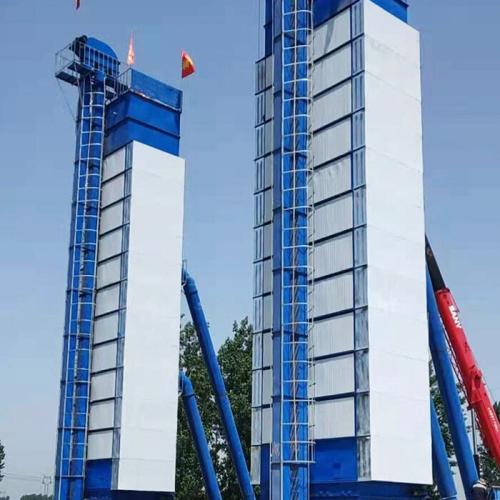
Tower Dryers
Click to view high-res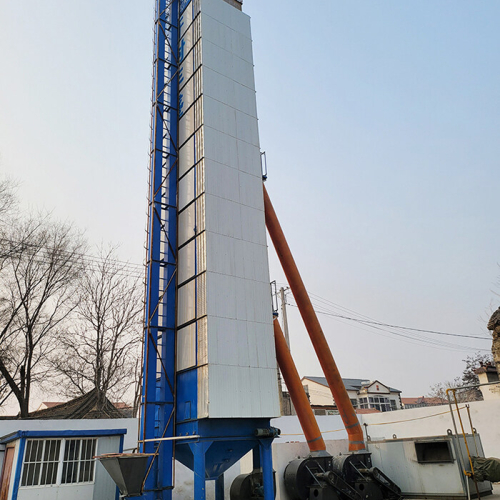
Tower Dryers
Click to view high-res
Tower Dryers
Click to view high-res
Tower Dryers
Click to view high-res50+ Years of Thermal Engineering Leadership.
Since 1976, Kerone Engineering Solutions has delivered over 5,000 custom-engineered thermal and process installations across 50+ countries. In technical collaboration with premier global institutions like CSIR-CEERI and University of Nottingham research partnerships, we design and manufacture high-efficiency machinery that minimizes production downtime and cuts operating expenses.
Unlike standard off-the-shelf equipment suppliers, Kerone operates a complete pilot-scale testing facility at our KRDC Ambernath center. We validate your exact raw material properties — determining moisture sorption isotherms, specific heat capacity, and dielectric behavior — before finalizing equipment sizing, ensuring zero risk during industrial scale-up.
Engineering precision, built into every system.
Energy-efficient Design
Energy-efficient design with advanced heat management.
Uniform Drying
Uniform drying with consistent temperature distribution.
Customizable Airflow and Heating
Customizable airflow and heating configurations.
Automatic Control Systems
Automatic control systems for precision and safety.
Robust Construction Ensuring
Robust construction ensuring long operational life.
Low Maintenance
Low maintenance with easy-to-clean components.
Ideal for Both Batch and
Ideal for both batch and continuous drying processes.
Optimized
Optimized for sensitive and bulk materials alike.
Powered by AI, Machine Learning & Smart IoT Integration
Modern industrial processing requires unprecedented thermal precision, energy efficiency, and operational agility. Kerone equips each system with high-speed industrial edge computing controllers, multi-spectral non-contact infrared pyrometry, and proprietary closed-loop machine learning algorithms that continuously analyze process parameters in real time.
The intelligent automation stack monitors dynamic changes in incoming material load, bed thickness, moisture content, and environmental factors. In response, our algorithms dynamically adjust heater power arrays, generator frequency, conveyor drive velocities, and exhaust dampers within milliseconds — entirely eliminating product burn, under-processing, or thermal hotspotting.
Seamlessly integrated with factory-wide SCADA and enterprise ERP architectures via native MQTT, OPC-UA, and Modbus TCP protocols, our systems deliver complete digital recipe control, remote diagnostics, predictive maintenance alerting, and tamper-evident batch logs compliant with global FDA 21 CFR Part 11 and cGMP standards.
Adaptive Heat Modulation
Neural algorithms detect material thermal variations in real time (<50ms response) and tune generator frequency and power arrays automatically.
IoT Cloud Telemetry
Continuous bidirectional telemetry stream via MQTT/OPC-UA protocols directly to centralized plant SCADA, MES, or mobile engineer dashboards.
Predictive Maintenance
Monitors magnetron cathode current, vibration frequency signatures, and differential filter pressure to schedule AMC maintenance before failures occur.
Quality & Batch Traceability
Automated digital recipe execution, multi-stage temperature ramp/soak curves, and cryptographically signed electronic batch logs compliant with 21 CFR Part 11.
Engineered for High-Value Industrial Sectors
Tailored thermal and process configurations across continuous manufacturing lines.
Food & Beverage
Drying fruits, vegetables, meat, fish, and herbs.
Agriculture
Moisture removal from grains, seeds, and crops.
Pharmaceutical
Drying herbal extracts, granules, and powders.
Chemical & Mineral
Processing catalysts, pigments, and minerals.
Industrial
Drying of ceramics, coal, polymers, and composites.
Configured to Your Process Window
Technical parameter envelopes across industrial manufacturing and engineering architectures.
Frequently Asked Questions
Engineering answers regarding equipment sizing, integration, and process performance.
Tower dryers are designed for free-flowing granular materials that can be fed from the top, flow downward under gravity through drying and cooling sections, and discharge from the bottom without bridging. Grains (wheat, maize, rice, sorghum), oilseeds, animal feed pellets, plastic granules, fertiliser prills, and coal briquettes are common materials. The critical material property is flowability, materials prone to bridging, clumping, or sticking at elevated temperatures require special discharge mechanisms such as counter-rotating rollers or agitating louvers. Material bulk density also determines the cross-sectional area required for a given mass flow rate through the tower.
A tower dryers is an industrial system that removes moisture from materials using controlled heat and airflow.
It operates by circulating hot air or transferring heat to evaporate moisture from products efficiently.
It ensures faster drying, energy efficiency, and product uniformity.
Industries like food, agriculture, pharmaceutical, and chemical commonly use these dryers.
Yes, Kerone designs every system according to specific industry and process needs.
Yes, precise temperature control ensures safe drying for sensitive materials.
Kerone’s designs optimize heat recovery and minimize energy consumption.
Regular inspection, cleaning, and calibration ensure optimal performance and longer lifespan.
Throughput and residence time in a tower dryer are controlled by the discharge mechanism at the base of the tower, which governs how quickly material flows through the drying column. Common discharge mechanisms include metering rolls, vibrating distributors, and motorised screw conveyors whose speed is adjusted by the PLC. A slower discharge rate increases residence time, giving the material longer exposure to the drying air, while a faster rate reduces it. The inlet temperature and airflow volume are the primary parameters adjusted to hit a target outlet moisture content at a given throughput. Tower dryers designed for grain drying typically include online moisture measurement in the discharge stream to provide feedback for discharge rate and temperature control.
Freshly harvested grain can arrive at the dryer with moisture content that varies from 18% to 30% or more depending on harvest conditions and crop variety. A fixed operating parameter setting would over-dry low-moisture grain or under-dry high-moisture grain. Modern tower dryers handle this variability through an inlet moisture sensor that measures incoming moisture continuously and transmits the data to the PLC. The control system then automatically adjusts discharge speed (residence time), inlet temperature, or both to compensate. For dryers without automated control, an experienced operator uses the inlet and outlet moisture measurements to manually adjust operating parameters. Consistent outlet moisture, typically 13–14% for safe grains of storage is the key performance target.
Fire and explosion risk are real concerns in grain tower dryers because grain dust is combustible. Essential safety provisions include a grain temperature monitoring system that triggers an automatic shutdown if the grain temperature exceeds a safe threshold, typically 60–65°C to avoid germination damage and 80°C to avoid ignition risk. Over-temperature alarms on the heating air supply, fire detection sensors in the drying column, and emergency water quench provisions are additional requirements. The burner management system must comply with EN 746 or equivalent. Rotary spreaders at the grain inlet should be designed to prevent foreign object damage. Dust collection and control at the discharge end prevent accumulation of explosive dust concentrations.
Yes. Most grain tower dryers are designed with dedicated drying zones and a cooling zone as an integrated section at the base of the tower. In the cooling zone, ambient air (or chilled air for sensitive materials) is blown through the material column in the same counterflow direction, removing sensible heat before discharge. This is important because hot grain discharged directly into storage can develop condensation when it contacts cooler air in the silo, which promotes mould growth. The height ratio between drying and cooling sections is determined by the drying duty and the required cooling delta-T. Separating these functions with distinct air inlet and exhaust ports allows independent control of drying and cooling air conditions.
For large-volume grain drying, tower dryers typically have lower operating cost per tonne than rotary drum dryers. The primary reason is thermal efficiency: counterflow tower dryers extract more heat from the drying air before it exhausts, compared to the concurrent or cross-flow airflow in many rotary designs. Tower dryers also have fewer rotating parts — no drum to turn — which reduces mechanical wear and electrical consumption from drive motors. Maintenance requirements are generally lower because the discharge mechanism is the main moving component. The trade-off is higher capital cost and more complex civil work for the tall structure, which makes rotary dryers more economical at smaller capacities or where existing building structures cannot support a tower installation.
Tower dryers can be scaled in capacity by increasing the cross-sectional area (widening or extending the drying column) or by adding additional tower units in parallel. Modular tower dryer designs allow new sections to be flanged onto existing columns to increase drying zone height, extending residence time without changing the discharge mechanism or foundation significantly. For larger capacity jumps, a second parallel tower with shared control infrastructure is the common approach. Kerone advises customers who anticipate capacity growth within 5–10 years to design the initial foundation, electrical infrastructure, and ducting with future expansion in mind, as retrofitting these elements later is more costly than provisioning them upfront.
Let’s Engineer the Right Process.
From application trials to full-scale production systems, our engineering team works with you to develop the right thermal processing solution for your material, throughput, and production requirements.