Heat Pump Dryers
With over four decades of expertise, Kerone has established itself as a global leader in designing and manufacturing heat pump dryers tailored to industrial needs.
Engineered precision for Heat Pump Dryers.
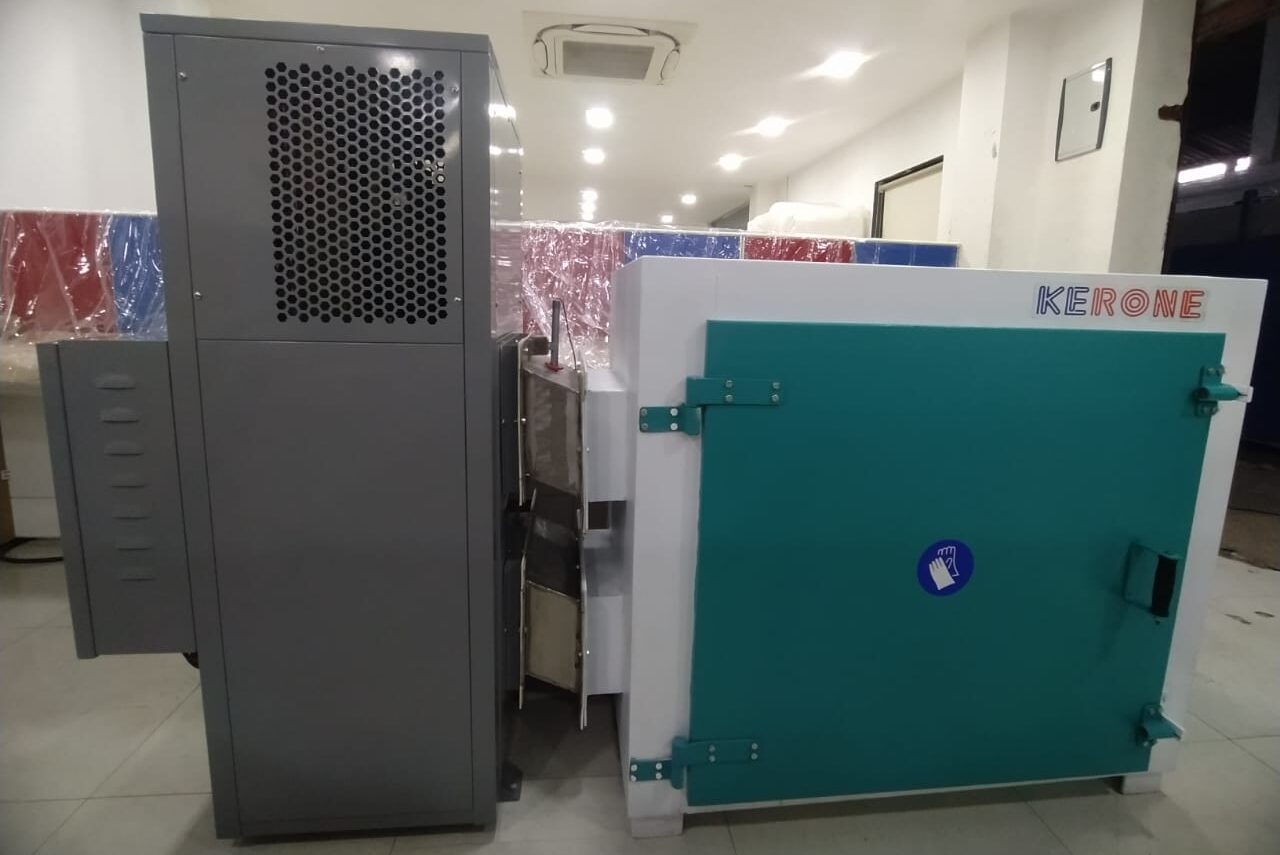
With over four decades of expertise, Kerone has established itself as a global leader in designing and manufacturing heat pump dryers tailored to industrial needs. The heat pump dryers is engineered to provide rapid and efficient drying through innovative heat transfer methods, ensuring precise moisture control and uniform output quality.
Kerone offers heat pump dryers or dehydrators for various food and agriculture processes, heat pump dryers provide ability to improve total dehydrating process by contracting the moisture from the drying air. It recycles the recovered heat to the dryers for heating, hence the energy is utilised in better manner and not wasted, heat is reutilised in more substantial manner instead of wasting it in atmosphere in any other type of dyers.
This results in drying of material at low temperature typically ranging from 60oF to 160oF (even upto 2000F for larger systems), low cost and also provides better results in humid conditions.
Our advanced AI, ML, and IoT technologies, this solution delivers smarter automation, real-time insights, and predictive intelligence to enhance efficiency and drive future-ready growth.
Continuous tracking of process parameters with instant adjustments.
Intelligent fault detection to prevent failures before they occur.
The thermodynamic architecture of our Heat Pump Dryers incorporates advanced thermal modeling and computational fluid dynamics (CFD) to ensure optimal heat and mass transfer across the entire processing zone. By precisely controlling thermal gradients, air velocity profiles, and direct energy delivery mechanisms, the system achieves uniform treatment while preventing localized overheating, product degradation, or thermal stress. This balance of intensive heat transfer and controlled retention time ensures maximum operational throughput with minimal specific energy consumption.
Built with heavy-duty structural engineering and sanitary metallurgy, each unit is manufactured to withstand continuous 24/7 industrial operating conditions. Contact surfaces are finished in high-grade stainless steel (SS 304, SS 316L, or corrosion-resistant alloys) with sanitary mirror-polish options, CIP/SIP washdown provisions, and hermetic chamber sealing. This guarantees full compliance with stringent international hygiene, CE machinery directives, and cGMP standards across food, pharmaceutical, specialty chemical, and heavy manufacturing applications.
Proprietary control algorithms ensure strict process repeatability, while built-in safety interlocks and electromagnetic shielding comply with international CE and OSHA standards. Full process development support — including material loss tangent testing, moisture sorption isotherms, and pilot trials at our Ambernath R&D facility — ensures the selected technology matches your exact industrial throughput goals.
Product & Systems Gallery
Explore authentic high-resolution photographs of industrial machinery, pilot trial rigs, and continuous turnkey processing installations engineered by Kerone Engineering Solutions for Heat Pump Dryers. Each system is fabricated at our ISO 9001:2015 certified manufacturing facilities with precision laser cutting, robotic welding, and stringent Factory Acceptance Testing (FAT).
Heat Pump Dryers
Click to view high-res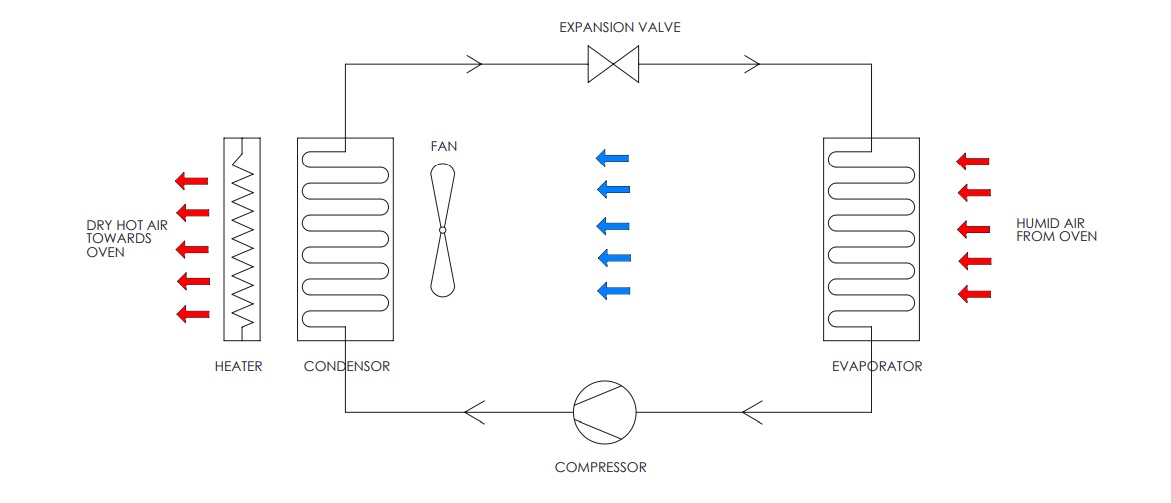
Heat Pump Dryers
Click to view high-res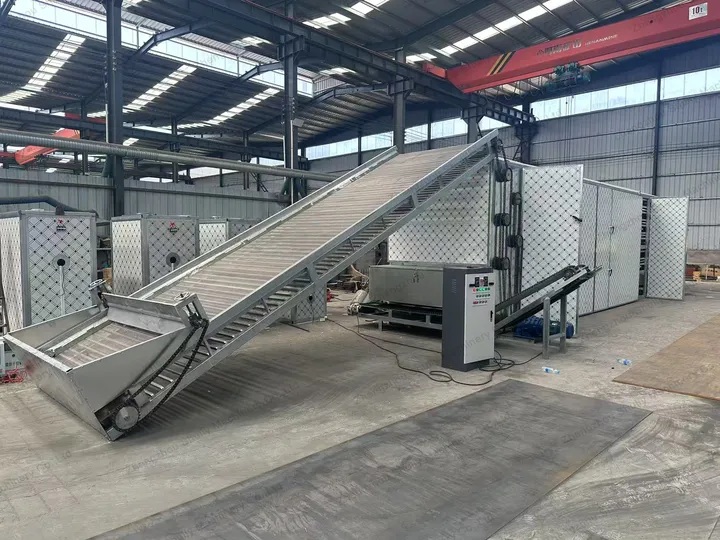
Heat Pump Dryers
Click to view high-res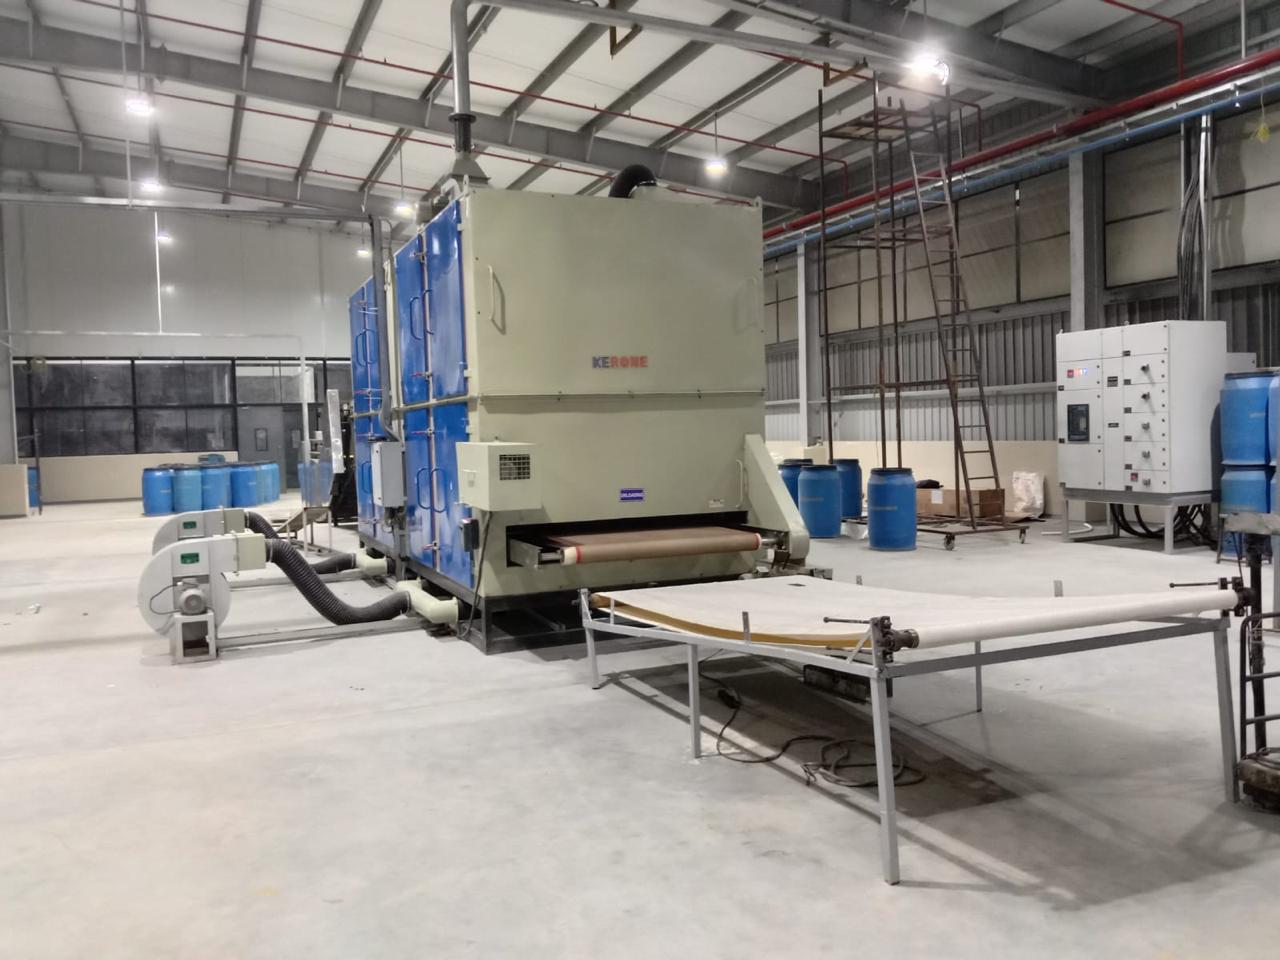
Heat Pump Dryers
Click to view high-res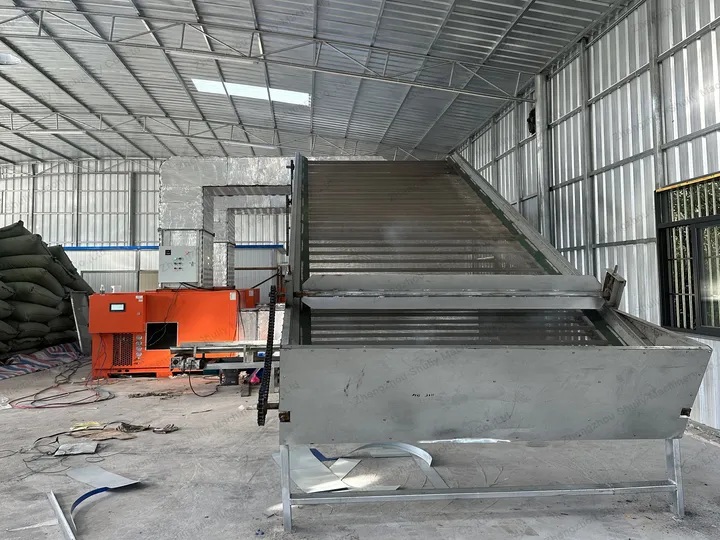
Heat Pump Dryers
Click to view high-res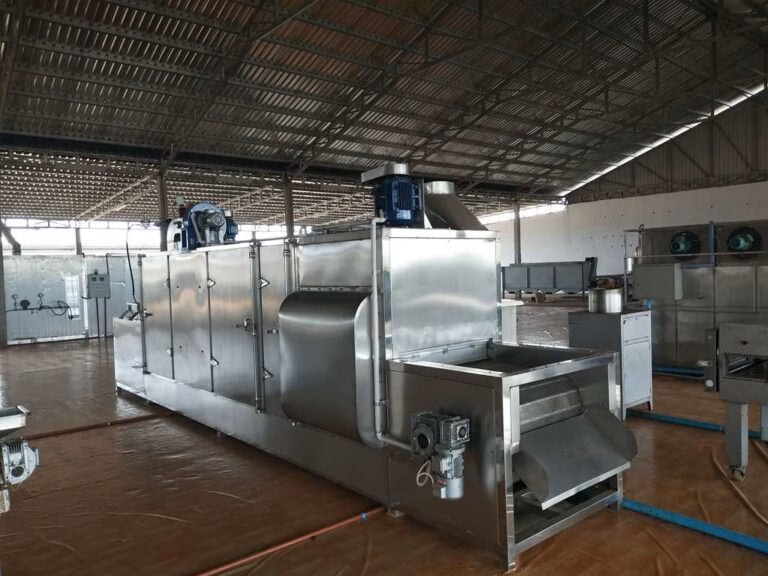
Heat Pump Dryers
Click to view high-res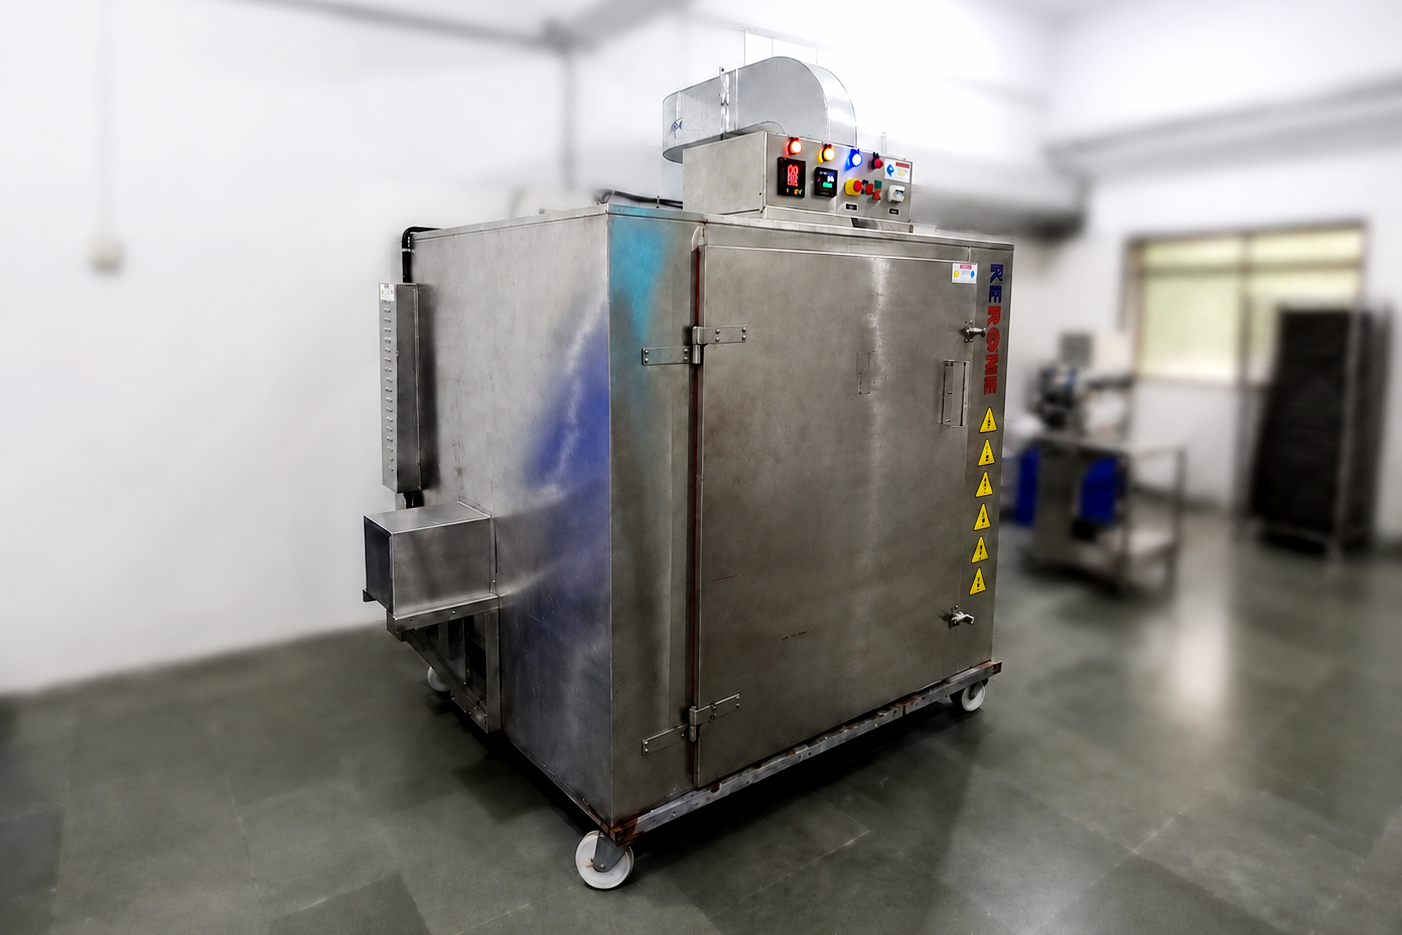
Heat Pump Dryers
Click to view high-res
Heat Pump Dryers
Click to view high-res
Heat Pump Dryers
Click to view high-res
Heat Pump Dryers
Click to view high-res
Heat Pump Dryers
Click to view high-res
Heat Pump Dryers
Click to view high-res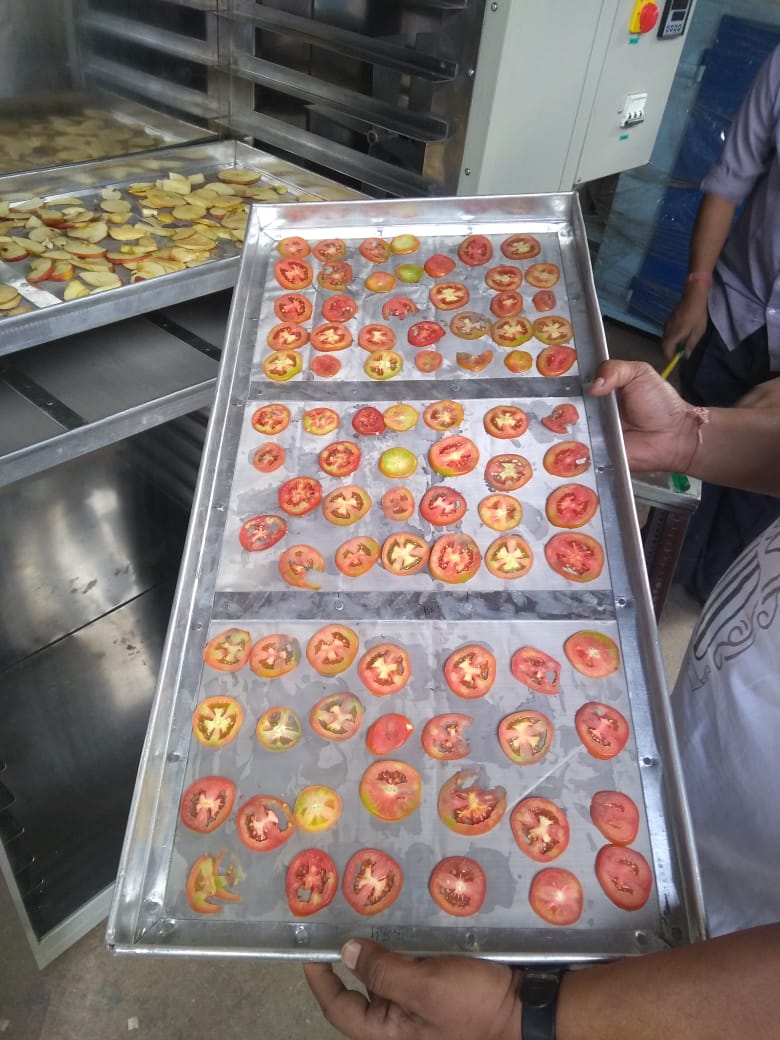
Heat Pump Dryers
Click to view high-res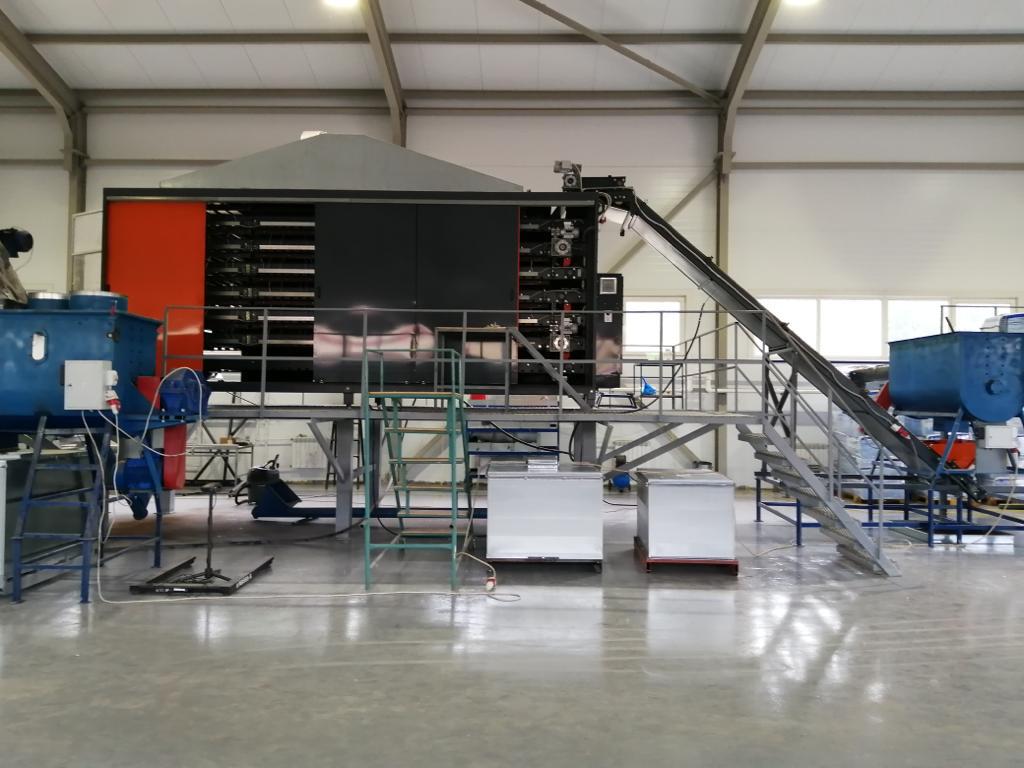
Heat Pump Dryers
Click to view high-res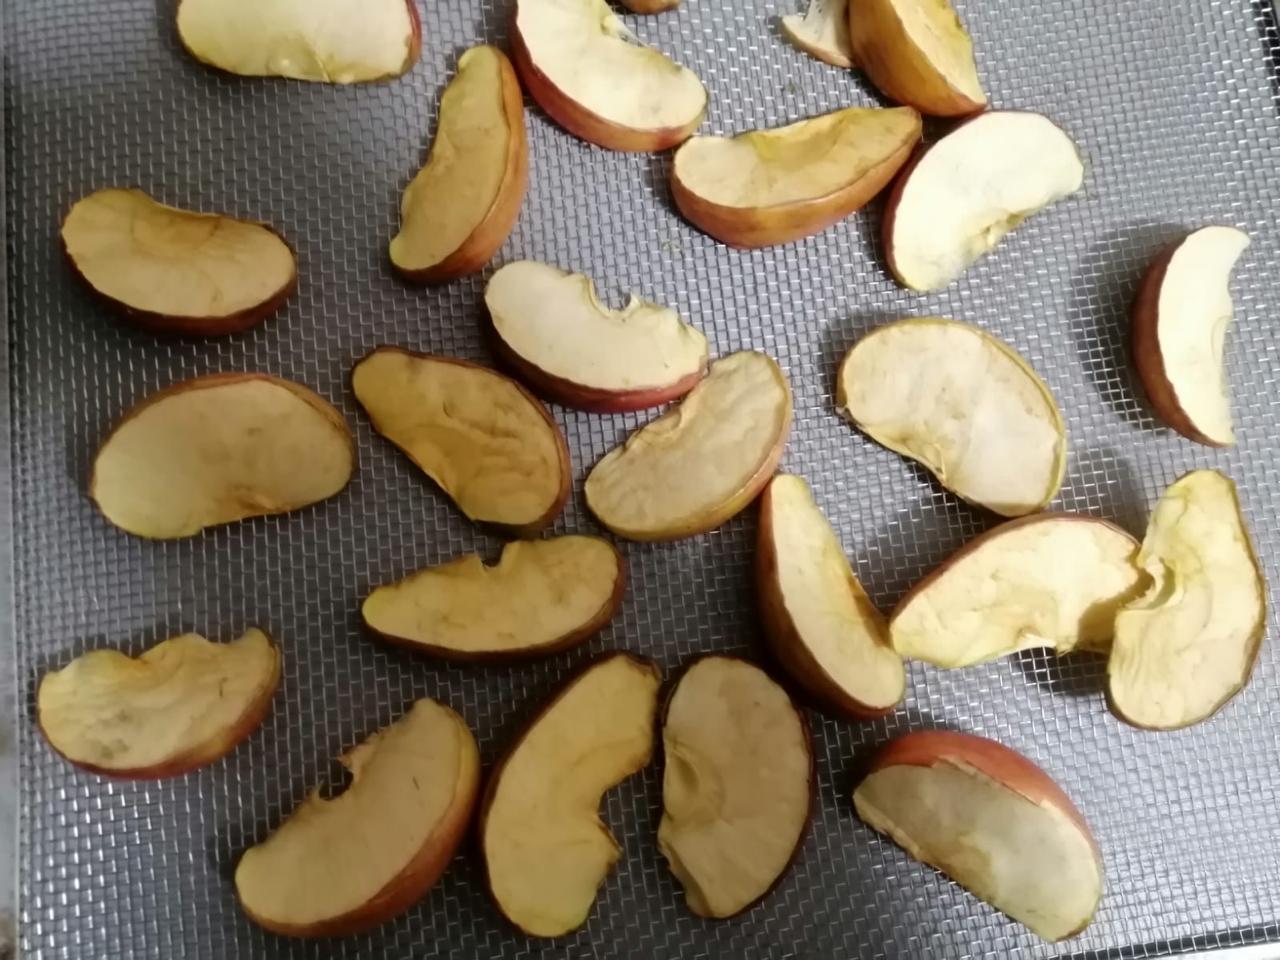
Heat Pump Dryers
Click to view high-res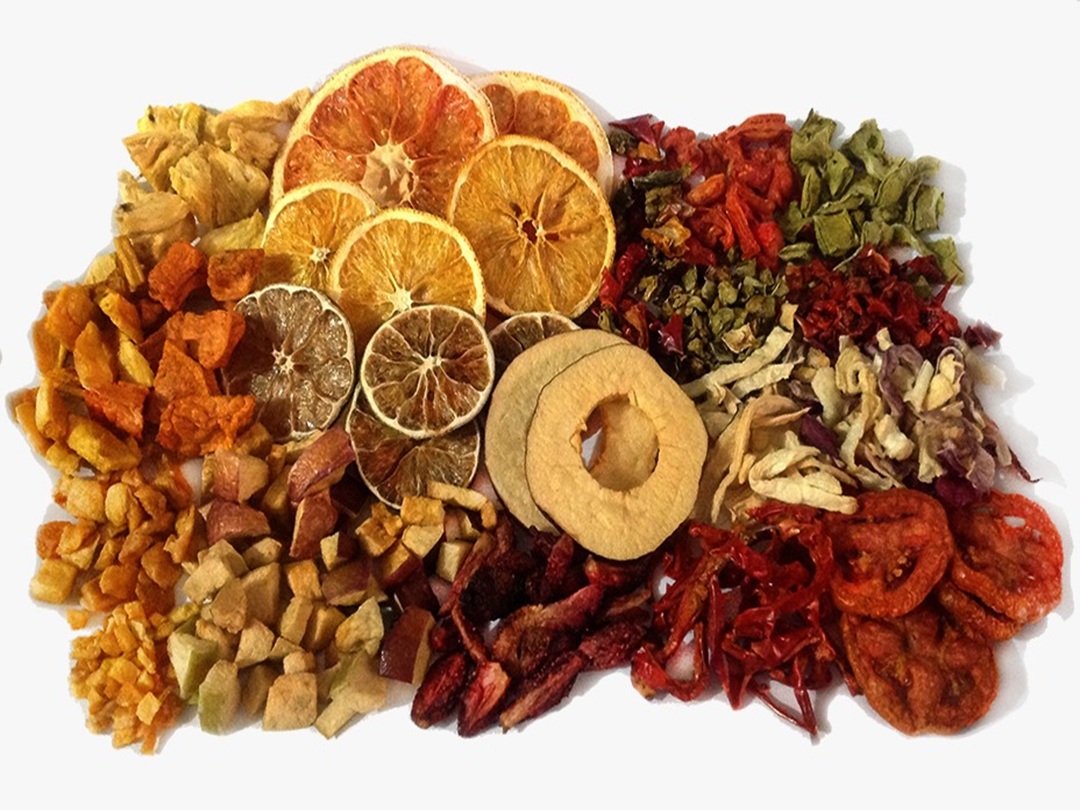
Heat Pump Dryers
Click to view high-res
Heat Pump Dryers
Click to view high-res
Heat Pump Dryers
Click to view high-res
Heat Pump Dryers
Click to view high-res50+ Years of Thermal Engineering Leadership.
Since 1976, Kerone Engineering Solutions has delivered over 5,000 custom-engineered thermal and process installations across 50+ countries. In technical collaboration with premier global institutions like CSIR-CEERI and University of Nottingham research partnerships, we design and manufacture high-efficiency machinery that minimizes production downtime and cuts operating expenses.
Unlike standard off-the-shelf equipment suppliers, Kerone operates a complete pilot-scale testing facility at our KRDC Ambernath center. We validate your exact raw material properties — determining moisture sorption isotherms, specific heat capacity, and dielectric behavior — before finalizing equipment sizing, ensuring zero risk during industrial scale-up.
Engineering precision, built into every system.
High Drying Rate
High drying rate with efficient heat transfer design.
Energy-efficient Operation
Energy-efficient operation with controlled temperature settings.
Ideal for Heat-sensitive and
Ideal for heat-sensitive and moisture-rich materials.
Fully Automated Operation
Fully automated operation with minimal manual intervention.
Robust Construction Suitable
Robust construction suitable for continuous operation.
Uniform Drying Ensuring Product
Uniform drying ensuring product consistency.
Flexible Design Adaptable
Flexible design adaptable for various industries.
Reduced Operational Downtime and
Reduced operational downtime and maintenance costs.
Powered by AI, Machine Learning & Smart IoT Integration
Modern industrial processing requires unprecedented thermal precision, energy efficiency, and operational agility. Kerone equips each system with high-speed industrial edge computing controllers, multi-spectral non-contact infrared pyrometry, and proprietary closed-loop machine learning algorithms that continuously analyze process parameters in real time.
The intelligent automation stack monitors dynamic changes in incoming material load, bed thickness, moisture content, and environmental factors. In response, our algorithms dynamically adjust heater power arrays, generator frequency, conveyor drive velocities, and exhaust dampers within milliseconds — entirely eliminating product burn, under-processing, or thermal hotspotting.
Seamlessly integrated with factory-wide SCADA and enterprise ERP architectures via native MQTT, OPC-UA, and Modbus TCP protocols, our systems deliver complete digital recipe control, remote diagnostics, predictive maintenance alerting, and tamper-evident batch logs compliant with global FDA 21 CFR Part 11 and cGMP standards.
Adaptive Heat Modulation
Neural algorithms detect material thermal variations in real time (<50ms response) and tune generator frequency and power arrays automatically.
IoT Cloud Telemetry
Continuous bidirectional telemetry stream via MQTT/OPC-UA protocols directly to centralized plant SCADA, MES, or mobile engineer dashboards.
Predictive Maintenance
Monitors magnetron cathode current, vibration frequency signatures, and differential filter pressure to schedule AMC maintenance before failures occur.
Quality & Batch Traceability
Automated digital recipe execution, multi-stage temperature ramp/soak curves, and cryptographically signed electronic batch logs compliant with 21 CFR Part 11.
Engineered for High-Value Industrial Sectors
Tailored thermal and process configurations across continuous manufacturing lines.
Food & Dairy
Milk powder, starch, coffee, and fruit pulp drying.
Chemical
Drying of pigments, catalysts, and polymer granules.
Pharmaceutical
Spray-drying of extracts and heat-sensitive drugs.
Textile
Dehydration of fruits, vegetables, powders, and herbs.
Agricultural
Drying of grains, seeds, and organic fertilizers.
Configured to Your Process Window
Technical parameter envelopes across industrial manufacturing and engineering architectures.
Frequently Asked Questions
Engineering answers regarding equipment sizing, integration, and process performance.
A heat pump dryers is a system that removes moisture using controlled heat and airflow for uniform drying results.
Heat pump dryers use a refrigeration cycle to extract latent heat from the moisture-laden exhaust air and transfer that recovered heat back into the incoming drying air, rather than generating all drying heat directly from electrical resistance or combustion. Because the system is moving and concentrating existing thermal energy rather than creating all of it from the electrical input, the ratio of heat delivered to electricity consumed, known as the coefficient of performance, can exceed one, often in the range of two to four depending on operating conditions. This isn't energy being created from nothing; it reflects that most of the delivered heat originates from recovered latent heat in the air stream, with electricity primarily driving the compressor that moves this heat rather than generating it directly, which is why the efficiency framing differs from simple electrical-to-heat conversion.
Heat pump dryers typically operate in a low to moderate temperature range, commonly between about 60 and 160 degrees Fahrenheit for most applications, with some larger systems extending toward 200 degrees Fahrenheit. This range suits heat-sensitive materials where higher-temperature conventional drying would cause case hardening, nutrient degradation, color change, or loss of volatile aromatic compounds, which is why fruits, vegetables, herbs, and certain pharmaceutical extracts are common applications. Materials that tolerate or require higher temperatures for effective moisture removal, such as some industrial minerals or coarse materials with primarily surface moisture, may not see the same relative benefit from heat pump technology compared with conventional higher-temperature drying methods, since the energy efficiency advantage is most pronounced specifically within this lower temperature operating window.
Conventional hot air dryers rely on the moisture-carrying capacity difference between ambient intake air and heated exhaust air, which diminishes significantly when ambient humidity is already high, since there's less room for the heated air to absorb additional moisture from the product before reaching saturation. Heat pump dryers operate in a more closed-loop or semi-closed configuration where the dehumidification happens mechanically through the refrigeration cycle's condensing coil rather than relying on ambient air's absorption capacity, which makes their drying performance comparatively more stable and less dependent on ambient humidity conditions. This is one of the most commonly cited advantages of heat pump drying in humid climates or during monsoon seasons where conventional drying slows considerably.
Energy savings vary considerably by product, target moisture removal, and operating conditions, but many heat pump dryer installations report energy consumption reductions in the range of 30 to 60 percent compared with conventional electric resistance or fossil-fuel-fired hot air drying for similar product types and final moisture targets. The wider end of this range tends to apply in humid ambient conditions where conventional drying efficiency drops most, while drier ambient conditions narrow the relative advantage somewhat since conventional drying performs comparatively better when ambient air already has good moisture-absorption capacity. Buyers should request energy consumption data based on trials with their specific product rather than relying solely on generic percentage claims, since product-specific drying curves significantly affect actual achieved savings.
Because heat pump drying typically operates in a more enclosed air loop with lower processing temperatures than conventional hot air drying, there's potential to capture and recover volatile compounds that would otherwise be lost to atmosphere through an open exhaust stream in conventional systems. This is particularly relevant for herbs, spices, and certain fruit products where aromatic compound retention significantly affects final product quality and market value. The recovery capability depends on the specific system design and whether condensate collection points are positioned to capture these volatiles rather than simply removing them as waste moisture, so this should be confirmed as a specific design feature rather than assumed as a default characteristic of all heat pump systems.
The refrigeration circuit introduces maintenance requirements not present in conventional electric or direct-fired dryers, including periodic refrigerant level checks, condenser and evaporator coil cleaning to prevent airflow restriction from product dust or residue buildup, and compressor servicing on a schedule similar to commercial refrigeration equipment. Coil cleaning frequency depends heavily on the product being dried, since dusty or fibrous materials accumulate on coil surfaces faster than clean, low-particulate products, reducing heat transfer efficiency if not addressed regularly. This additional maintenance category is a genuine trade-off against the energy savings heat pump technology offers, and operators should factor refrigeration system servicing into total cost of ownership comparisons rather than evaluating purchase price and energy savings alone.
It operates through a process of heat transfer and air circulation to evaporate moisture from materials efficiently.
It provides high efficiency, uniform drying, and low energy consumption.
Industries such as food, chemical, pharmaceutical, and textile rely heavily on these dryers.
Yes, Kerone designs systems tailored to specific process and material needs.
The design ensures quick cleaning and minimal servicing requirements.
Kerone’s systems are optimized for reduced power consumption and higher heat utilization.
Fruits, vegetables, spices, seafood, medicinal plants, and organic materials.
Yes, they reduce carbon emissions through energy recovery and reduced heat loss.

Let’s Engineer the Right Process.
From application trials to full-scale production systems, our engineering team works with you to develop the right thermal processing solution for your material, throughput, and production requirements.