Continuous Microwave Hybrid Heating Systems
Continuous Microwave Hybrid Heating Systems represent a breakthrough in industrial thermal processing technology, seamlessly combining microwave energy with conventional heating methods — such as hot air, infrared, or steam — to deliver unmatched heating uniformity, speed, and energy efficiency in a single, integrated production line.
Engineered precision for Continuous Microwave Hybrid Heating Systems.
Continuous Microwave Hybrid Heating Systems represent a breakthrough in industrial thermal processing technology, seamlessly combining microwave energy with conventional heating methods — such as hot air, infrared, or steam — to deliver unmatched heating uniformity, speed, and energy efficiency in a single, integrated production line.
Unlike conventional batch heating systems, these advanced solutions operate on a fully continuous conveyor-based mechanism, enabling round-the-clock processing without interruption. By coupling microwave’s deep volumetric penetration with the surface-finishing capability of supplementary heat sources, the hybrid system eliminates the common challenges of uneven heating, case hardening, and thermal runaway that often plague standalone microwave setups.
Engineered for demanding industrial environments, Kerone’s Continuous Microwave Hybrid Heating Systems offer precise temperature control, programmable power profiles, and real-time monitoring, making them the preferred choice for food processing, pharmaceuticals, chemicals, ceramics, rubber, and advanced material manufacturing across global industries.
Our advanced AI, ML, and IoT technologies, this solution delivers smarter automation, real-time insights, and predictive intelligence to enhance efficiency and drive future-ready growth.
Continuous tracking of process parameters with instant adjustments.
Intelligent fault detection to prevent failures before they occur.
Dynamic tuning of operations for maximum output and efficiency.
The thermodynamic architecture of our Continuous Microwave Hybrid Heating Systems incorporates advanced thermal modeling and computational fluid dynamics (CFD) to ensure optimal heat and mass transfer across the entire processing zone. By precisely controlling thermal gradients, air velocity profiles, and direct energy delivery mechanisms, the system achieves uniform treatment while preventing localized overheating, product degradation, or thermal stress. This balance of intensive heat transfer and controlled retention time ensures maximum operational throughput with minimal specific energy consumption.
Built with heavy-duty structural engineering and sanitary metallurgy, each unit is manufactured to withstand continuous 24/7 industrial operating conditions. Contact surfaces are finished in high-grade stainless steel (SS 304, SS 316L, or corrosion-resistant alloys) with sanitary mirror-polish options, CIP/SIP washdown provisions, and hermetic chamber sealing. This guarantees full compliance with stringent international hygiene, CE machinery directives, and cGMP standards across food, pharmaceutical, specialty chemical, and heavy manufacturing applications.
Proprietary control algorithms ensure strict process repeatability, while built-in safety interlocks and electromagnetic shielding comply with international CE and OSHA standards. Full process development support — including material loss tangent testing, moisture sorption isotherms, and pilot trials at our Ambernath R&D facility — ensures the selected technology matches your exact industrial throughput goals.
Product & Systems Gallery
Explore authentic high-resolution photographs of industrial machinery, pilot trial rigs, and continuous turnkey processing installations engineered by Kerone Engineering Solutions for Continuous Microwave Hybrid Heating Systems. Each system is fabricated at our ISO 9001:2015 certified manufacturing facilities with precision laser cutting, robotic welding, and stringent Factory Acceptance Testing (FAT).
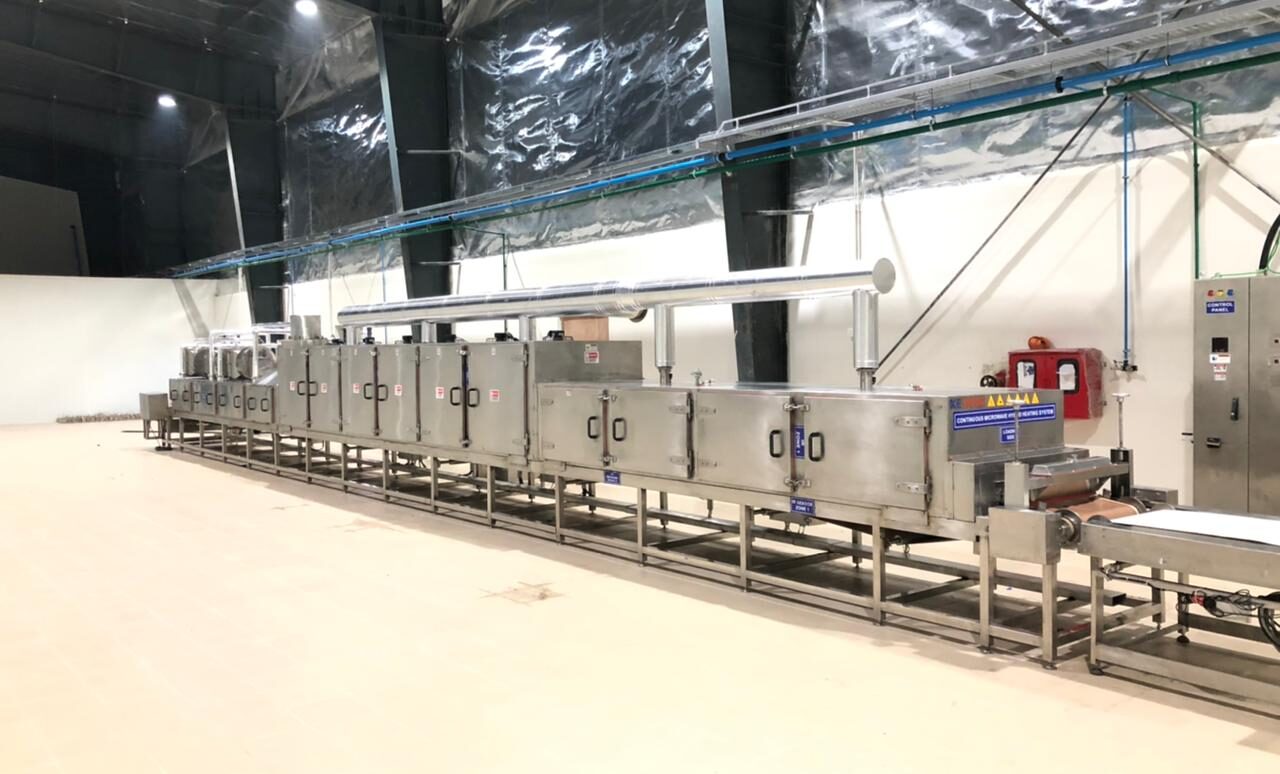
Continuous Microwave Hybrid Heating Systems
Click to view high-res
Continuous Microwave Hybrid Heating Systems
Click to view high-res
Continuous Microwave Hybrid Heating Systems
Click to view high-res
Continuous Microwave Hybrid Heating Systems
Click to view high-res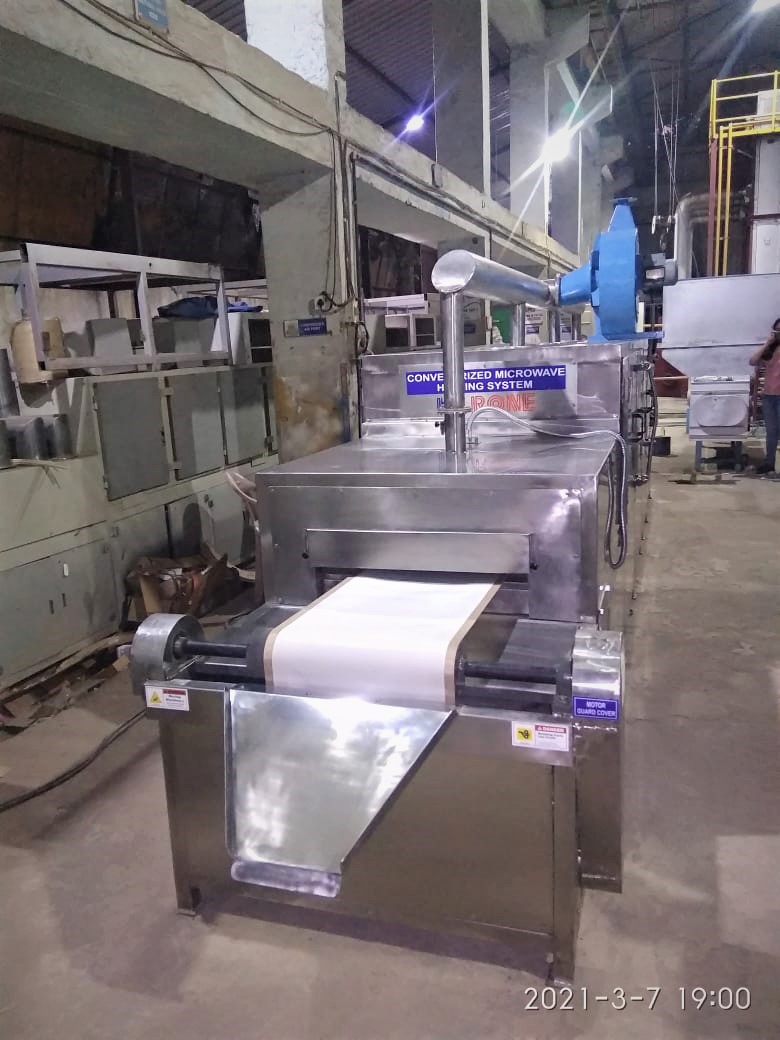
Continuous Microwave Hybrid Heating Systems
Click to view high-res
Continuous Microwave Hybrid Heating Systems
Click to view high-res50+ Years of Thermal Engineering Leadership.
Since 1976, Kerone Engineering Solutions has delivered over 5,000 custom-engineered thermal and process installations across 50+ countries. In technical collaboration with premier global institutions like CSIR-CEERI and University of Nottingham research partnerships, we design and manufacture high-efficiency machinery that minimizes production downtime and cuts operating expenses.
Unlike standard off-the-shelf equipment suppliers, Kerone operates a complete pilot-scale testing facility at our KRDC Ambernath center. We validate your exact raw material properties — determining moisture sorption isotherms, specific heat capacity, and dielectric behavior — before finalizing equipment sizing, ensuring zero risk during industrial scale-up.
Engineering precision, built into every system.
Minimal Human Intervention
Continuous conveyor-based operation enabling 24/7 uninterrupted high-throughput industrial production with minimal human intervention
Multi-zone Independent Microwave
Multi-zone independent microwave power control allowing precise customisation of heat profiles across different sections of the processing tunnel
Industry 4.0 Readiness
Advanced SCADA and PLC automation with real-time temperature monitoring, data logging, and remote diagnostics for Industry 4.0 readiness
Stainless Steel GMP/food-grade
Stainless steel GMP/food-grade construction with hygienic belt design, easy clean-in-place (CIP) access, and full IP65-rated enclosures
Energy-efficient Microwave Magnetrons
Energy-efficient microwave magnetrons with solid-state power supply options, reducing energy consumption by up to 40–60% versus conventional heating alone
Integrated Exhaust, Moisture
Integrated exhaust, moisture management, and vapour extraction systems ensuring safe, compliant, and consistent processing environments
Powered by AI, Machine Learning & Smart IoT Integration
Modern industrial processing requires unprecedented thermal precision, energy efficiency, and operational agility. Kerone equips each system with high-speed industrial edge computing controllers, multi-spectral non-contact infrared pyrometry, and proprietary closed-loop machine learning algorithms that continuously analyze process parameters in real time.
The intelligent automation stack monitors dynamic changes in incoming material load, bed thickness, moisture content, and environmental factors. In response, our algorithms dynamically adjust heater power arrays, generator frequency, conveyor drive velocities, and exhaust dampers within milliseconds — entirely eliminating product burn, under-processing, or thermal hotspotting.
Seamlessly integrated with factory-wide SCADA and enterprise ERP architectures via native MQTT, OPC-UA, and Modbus TCP protocols, our systems deliver complete digital recipe control, remote diagnostics, predictive maintenance alerting, and tamper-evident batch logs compliant with global FDA 21 CFR Part 11 and cGMP standards.
Adaptive Heat Modulation
Neural algorithms detect material thermal variations in real time (<50ms response) and tune generator frequency and power arrays automatically.
IoT Cloud Telemetry
Continuous bidirectional telemetry stream via MQTT/OPC-UA protocols directly to centralized plant SCADA, MES, or mobile engineer dashboards.
Predictive Maintenance
Monitors magnetron cathode current, vibration frequency signatures, and differential filter pressure to schedule AMC maintenance before failures occur.
Quality & Batch Traceability
Automated digital recipe execution, multi-stage temperature ramp/soak curves, and cryptographically signed electronic batch logs compliant with 21 CFR Part 11.
Engineered for High-Value Industrial Sectors
Tailored thermal and process configurations across continuous manufacturing lines.
Food Industry
Drying fruits, vegetables, powders, and herbs.
Chemical Industry
Processing pigments, catalysts, and polymers.
Pharmaceutical
Drying granules, herbal extracts, and formulations.
Industrial
Surface treatment, coatings, and composite material drying.
Configured to Your Process Window
Technical parameter envelopes across industrial manufacturing and engineering architectures.
Frequently Asked Questions
Engineering answers regarding equipment sizing, integration, and process performance.
A Continuous Microwave Hybrid Heating System is an industrial-grade processing line that combines microwave energy with one or more conventional heat sources — such as hot air, infrared, or steam — operating continuously via a conveyor belt. Unlike a conventional microwave oven, which is a batch-mode device designed for small volumes, a hybrid system processes material at scale without stopping, delivers multi-mode heating for superior uniformity, and is fully automated with industrial control systems suitable for 24/7 manufacturing environments.
Kerone's systems are available in both 915 MHz and 2450 MHz microwave frequencies. The 915 MHz frequency offers deeper penetration and is preferred for thicker, denser materials such as meat blocks or large ceramic components. The 2450 MHz frequency is better suited for thin or moisture-rich products like snack foods, grains, and pharmaceutical granules. Kerone's engineers recommend the appropriate frequency — or a switchable dual-frequency configuration — based on your product's dielectric properties and required penetration depth.
In most industrial applications, Kerone's Continuous Microwave Hybrid Heating Systems deliver energy savings of 40–60% compared to purely conventional heating methods such as hot air ovens or steam tunnels. This saving arises because microwaves heat the product volumetrically and directly — not the surrounding air or chamber — resulting in dramatically lower heat losses. The exact saving depends on the product type, moisture content, throughput, and the specific hybrid configuration deployed.
Yes. Kerone designs and manufactures Continuous Microwave Hybrid Heating Systems to comply with GMP (Good Manufacturing Practice), FDA guidelines, and food-grade hygiene standards. All product-contact surfaces are constructed from 304 or 316L stainless steel, with hygienic conveyor belts, CIP-compatible (clean-in-place) designs, and full IP65 enclosures to prevent contamination. Systems for pharmaceutical applications can additionally be supplied with 21 CFR Part 11-compliant data logging and audit trail capabilities.
Safety is a fundamental design criterion for every Kerone system. Continuous Microwave Hybrid Heating Systems incorporate multiple layers of protection including microwave leakage suppression chokes at conveyor entry and exit points, interlock switches that instantly cut microwave power if a door or panel is opened, over-temperature and over-power protection circuits, earthing and shielding to international EMC standards, and integrated fire suppression readiness. All systems are CE-marked and can be supplied with ATEX certification for use in potentially explosive atmospheres.
Timeline varies with system complexity and customization level, but the general sequence includes initial process consultation and feasibility assessment, pilot trial runs on representative product samples if dielectric or thermal behavior is not already well characterized, detailed engineering design, fabrication, factory testing, shipping, and on-site installation and commissioning. Standard or near-standard configurations move through this sequence faster than fully custom multi-zone systems requiring extensive trial work. Customers with urgent capacity needs should engage Kerone's engineering team early in their capital planning process, since pilot trials and detailed design typically represent the largest variable in overall project timeline.
Case hardening occurs when the product surface dries and forms a dense, low-permeability layer before the core has finished releasing moisture, trapping internal moisture and slowing the remainder of the drying process while creating an inconsistent final product. In standalone microwave systems, this can happen if internal moisture migrates to the surface faster than it evaporates, especially with thick or dense products. Hybrid systems address this by using the conventional heat source, typically hot air, to actively manage surface conditions and promote consistent evaporation at the boundary layer while microwave energy continues driving moisture from the core outward, keeping the surface from forming an impermeable barrier before the interior is fully processed.
Line speed is calculated backward from the required residence time in the heating tunnel, which itself depends on product thickness, target moisture or temperature change, and the combined heating contribution from both the microwave and conventional heat zones. Thicker or denser products require longer residence time and therefore slower line speed for a given tunnel length, while thin or highly microwave-responsive products can be processed at higher speeds. Kerone's process engineers typically run pilot trials measuring temperature and moisture profiles at several line speeds before finalizing the production-scale conveyor speed and corresponding tunnel length needed to hit target throughput.
A multi-zone system divides the heating tunnel into independently controllable sections, each with its own power setting, allowing the heating profile to be shaped along the length of the tunnel rather than applying uniform energy throughout. This is valuable because optimal heating intensity often differs between the initial moisture removal phase and the final temperature equalization phase of a process. Single fixed-power tunnels apply the same energy density throughout, which can work for simple, uniform products but limits the ability to fine-tune the process for materials that need a different energy profile at different stages of treatment, such as products requiring gentle initial heating followed by a more intensive finishing zone.
SCADA and PLC connectivity allows production data, including temperature profiles, power consumption, and line speed, to be logged automatically and made available for remote monitoring rather than relying on manual operator logs. This data supports faster root-cause analysis when a quality deviation occurs, since engineers can review the exact process conditions for the affected batch rather than reconstructing events after the fact. Remote diagnostics also allow Kerone's service team to review system performance data and flag developing issues, such as gradually increasing reflected power indicating a component nearing end of life, before they cause an unplanned production stoppage.
Variable incoming moisture is managed primarily through adaptive power control, where temperature or moisture sensors positioned along the tunnel feed real-time data back to the control system, which adjusts microwave power in response rather than running a fixed program regardless of input variation. This closed-loop approach prevents underprocessing high-moisture batches or overprocessing drier ones, both of which would otherwise create inconsistent finished product quality. For products with highly variable raw material characteristics, such as seasonal agricultural inputs, this adaptive capability is often a more important specification than peak throughput, since consistent output quality depends on the system's ability to respond to incoming variability rather than just its rated capacity.
With proper maintenance, the structural and conveyor components of a hybrid system commonly remain in service for fifteen to twenty years or more, while microwave generation components such as magnetrons have a defined operating-hour lifespan and are treated as scheduled replacement items rather than structural components. System lifespan is most influenced by duty cycle intensity, the corrosiveness or abrasiveness of the product being processed, and how consistently scheduled maintenance is performed on seals, bearings, and electrical components. Facilities that follow Kerone's recommended preventive maintenance schedule and address minor component wear before it cascades into bigger failures typically extend useful equipment life well beyond facilities that defer maintenance until a breakdown forces action.
Let’s Engineer the Right Process.
From application trials to full-scale production systems, our engineering team works with you to develop the right thermal processing solution for your material, throughput, and production requirements.