Engineering Capability Overview & Design Philosophy
Kerone’s Engineering Capability Overview & Design Philosophy reflects decades of experience in delivering world-class industrial processing solutions across a diverse range of industries and technologies.
Engineered precision for Engineering Capability Overview & Design Philosophy.
Kerone’s Engineering Capability Overview & Design Philosophy reflects decades of experience in delivering world-class industrial processing solutions across a diverse range of industries and technologies. At its core, Kerone’s engineering approach is built on the principles of precision, innovation, sustainability, and customer-centric design.
Kerone’s multi-disciplinary engineering teams—comprising process engineers, mechanical designers, electrical and instrumentation engineers, and software developers—collaborate seamlessly to translate complex customer requirements into reliable, efficient, and future-proof engineering solutions.
From the first conceptual sketch to the final commissioning test, every Kerone project is executed with rigor, expertise, and a commitment to excellence.
Our advanced AI, ML, and IoT technologies, this solution delivers smarter automation, real-time insights, and predictive intelligence to enhance efficiency and drive future-ready growth.
Continuous tracking of process parameters with instant adjustments.
Intelligent fault detection to prevent failures before they occur.
Dynamic tuning of operations for maximum output and efficiency.
The thermodynamic architecture of our Engineering Capability Overview & Design Philosophy incorporates advanced thermal modeling and computational fluid dynamics (CFD) to ensure optimal heat and mass transfer across the entire processing zone. By precisely controlling thermal gradients, air velocity profiles, and direct energy delivery mechanisms, the system achieves uniform treatment while preventing localized overheating, product degradation, or thermal stress. This balance of intensive heat transfer and controlled retention time ensures maximum operational throughput with minimal specific energy consumption.
Built with heavy-duty structural engineering and sanitary metallurgy, each unit is manufactured to withstand continuous 24/7 industrial operating conditions. Contact surfaces are finished in high-grade stainless steel (SS 304, SS 316L, or corrosion-resistant alloys) with sanitary mirror-polish options, CIP/SIP washdown provisions, and hermetic chamber sealing. This guarantees full compliance with stringent international hygiene, CE machinery directives, and cGMP standards across food, pharmaceutical, specialty chemical, and heavy manufacturing applications.
Proprietary control algorithms ensure strict process repeatability, while built-in safety interlocks and electromagnetic shielding comply with international CE and OSHA standards. Full process development support — including material loss tangent testing, moisture sorption isotherms, and pilot trials at our Ambernath R&D facility — ensures the selected technology matches your exact industrial throughput goals.
Product & Systems Gallery
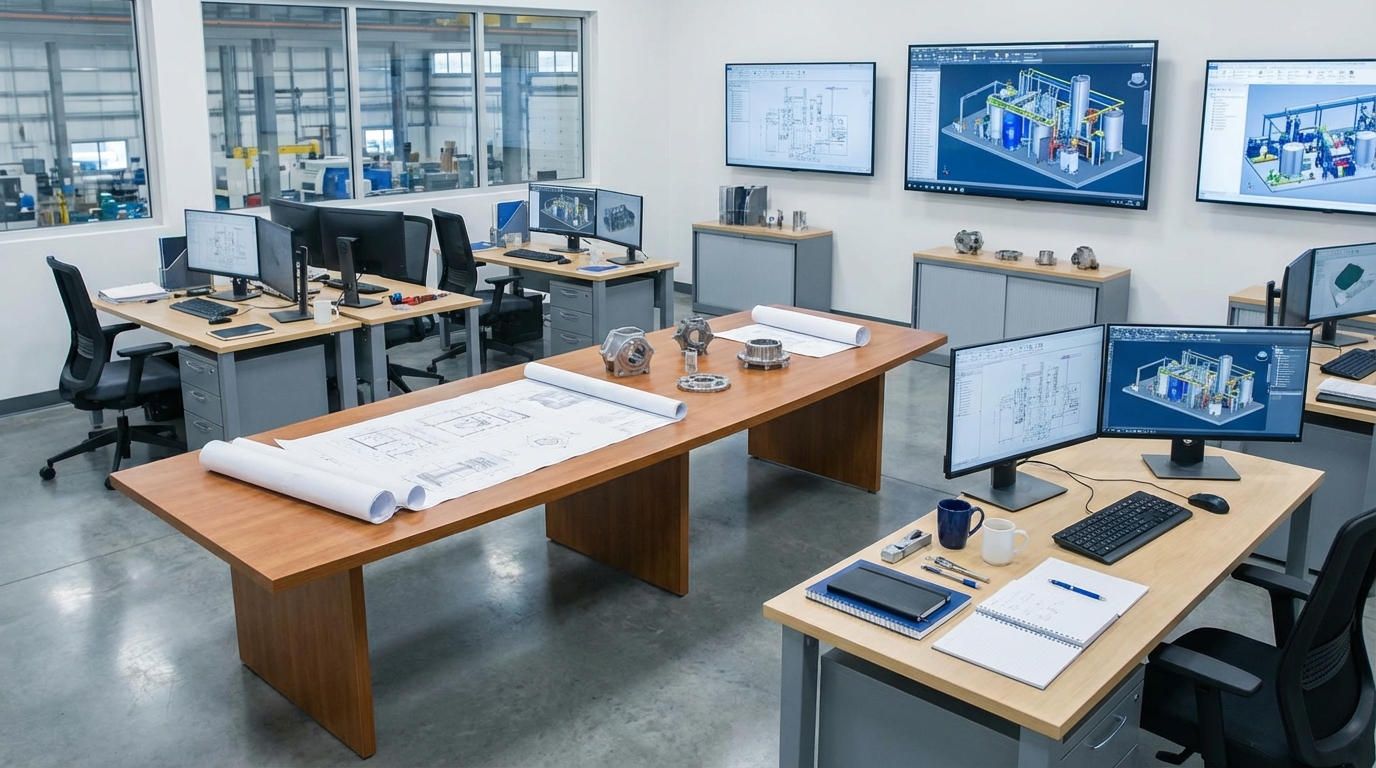
Explore authentic high-resolution photographs of industrial machinery, pilot trial rigs, and continuous turnkey processing installations engineered by Kerone Engineering Solutions for Engineering Capability Overview & Design Philosophy. Each system is fabricated at our ISO 9001:2015 certified manufacturing facilities with precision laser cutting, robotic welding, and stringent Factory Acceptance Testing (FAT).
Engineering Capability Overview & Design Philosophy
Click to view high-res
Engineering Capability Overview & Design Philosophy
Click to view high-res
Engineering Capability Overview & Design Philosophy
Click to view high-res
Engineering Capability Overview & Design Philosophy
Click to view high-res
Engineering Capability Overview & Design Philosophy
Click to view high-res
Engineering Capability Overview & Design Philosophy
Click to view high-res50+ Years of Thermal Engineering Leadership.
Since 1976, Kerone Engineering Solutions has delivered over 5,000 custom-engineered thermal and process installations across 50+ countries. In technical collaboration with premier global institutions like CSIR-CEERI and University of Nottingham research partnerships, we design and manufacture high-efficiency machinery that minimizes production downtime and cuts operating expenses.
Unlike standard off-the-shelf equipment suppliers, Kerone operates a complete pilot-scale testing facility at our KRDC Ambernath center. We validate your exact raw material properties — determining moisture sorption isotherms, specific heat capacity, and dielectric behavior — before finalizing equipment sizing, ensuring zero risk during industrial scale-up.
Engineering precision, built into every system.
Multi-disciplinary In-house
Multi-disciplinary in-house engineering across process, mechanical, electrical, and software disciplines
Advanced Design Tools
Advanced design tools including CFD, FEA, 3D CAD, and dynamic process simulation
ISO 9001 Certified Quality
ISO 9001 certified quality management system with rigorous design review and approval processes
Application of International Standards
ASME, IEC, ATEX, CE, GMP, EHEDG, and IS codes
Life-cycle Engineering
Life-cycle engineering philosophy prioritizing durability, maintainability, and energy efficiency
HAZOP and SIL Assessment Capability
HAZOP and SIL assessment capability for safe design of hazardous industrial processes
Integrated Project Management
Integrated project management with milestone tracking, risk management, and client reporting
Post-commissioning Support
Post-commissioning support including performance validation, operator training, and continuous improvement
Powered by AI, Machine Learning & Smart IoT Integration
Modern industrial processing requires unprecedented thermal precision, energy efficiency, and operational agility. Kerone equips each system with high-speed industrial edge computing controllers, multi-spectral non-contact infrared pyrometry, and proprietary closed-loop machine learning algorithms that continuously analyze process parameters in real time.
The intelligent automation stack monitors dynamic changes in incoming material load, bed thickness, moisture content, and environmental factors. In response, our algorithms dynamically adjust heater power arrays, generator frequency, conveyor drive velocities, and exhaust dampers within milliseconds — entirely eliminating product burn, under-processing, or thermal hotspotting.
Seamlessly integrated with factory-wide SCADA and enterprise ERP architectures via native MQTT, OPC-UA, and Modbus TCP protocols, our systems deliver complete digital recipe control, remote diagnostics, predictive maintenance alerting, and tamper-evident batch logs compliant with global FDA 21 CFR Part 11 and cGMP standards.
Adaptive Heat Modulation
Neural algorithms detect material thermal variations in real time (<50ms response) and tune generator frequency and power arrays automatically.
IoT Cloud Telemetry
Continuous bidirectional telemetry stream via MQTT/OPC-UA protocols directly to centralized plant SCADA, MES, or mobile engineer dashboards.
Predictive Maintenance
Monitors magnetron cathode current, vibration frequency signatures, and differential filter pressure to schedule AMC maintenance before failures occur.
Quality & Batch Traceability
Automated digital recipe execution, multi-stage temperature ramp/soak curves, and cryptographically signed electronic batch logs compliant with 21 CFR Part 11.
Engineered for High-Value Industrial Sectors
Tailored thermal and process configurations across continuous manufacturing lines.
Design and delivery of custom indus...
Design and delivery of custom industrial dryers, ovens, and thermal processing systems
Complete process plant engineering ...
Complete process plant engineering for chemical, pharmaceutical, and food industries
Smart factory and Industry 4.0 solu...
Smart factory and Industry 4.0 solution engineering for manufacturing modernization projects
Environmental engineering for pollu...
Environmental engineering for pollution control, waste treatment, and sustainability programs
Biochar and renewable energy system...
Biochar and renewable energy system engineering for carbon-neutral processing
Advanced material and surface engin...
Advanced material and surface engineering system design for high-performance applications
Configured to Your Process Window
Technical parameter envelopes across industrial manufacturing and engineering architectures.
Frequently Asked Questions
Engineering answers regarding equipment sizing, integration, and process performance.
Kerone has in-house expertise in process engineering, mechanical design, electrical and instrumentation engineering, civil and structural engineering, software and automation development, and project management.
Kerone uses industry-leading software including AutoCAD, SolidWorks, ANSYS (CFD and FEA), Aspen Plus for process simulation, MATLAB, and various PLC/SCADA programming environments.
Yes, Kerone operates under an ISO 9001 certified quality management system that governs all engineering, procurement, fabrication, and project delivery activities.
Kerone employs formal risk management methodologies including HAZOP, Failure Mode Effects Analysis (FMEA), and risk registers updated throughout the project lifecycle.
Sustainability is embedded in Kerone's design philosophy through energy efficiency optimization, waste minimization, use of renewable energy sources, and environmental compliance in every project.
Yes, Kerone designs to ASME, IEC, ATEX, CE, EHEDG, GMP, FDA, CPCB, IS, and other applicable international and regional standards depending on project location and industry.
Kerone uses an integrated project management framework with a dedicated project manager, cross-discipline coordination meetings, and digital collaboration tools to ensure seamless execution of complex projects.
Kerone provides post-commissioning performance validation, operator training, spare parts supply, preventive maintenance support, and ongoing process optimization consulting for all delivered projects.
Client process knowledge is essential input that Kerone's engineers cannot fully replicate independently, including material behavior quirks, operational constraints from existing facility layout, and lessons learned from previous equipment that should inform the new design. Design review meetings at key milestones give clients the opportunity to validate that the engineering direction matches their actual operational needs before detailed design and fabrication commitment lock in those decisions. Clients providing representative material samples for testing, when available, significantly improves design confidence compared to relying solely on written material specifications. Active client involvement during commissioning, including operator participation in performance validation testing, also improves the smoothness of the handover to routine production operation. Projects with engaged, responsive client technical contacts throughout the design phase consistently experience fewer late-stage surprises than projects where client involvement is minimal until commissioning.
Kerone maintains proven design platforms for core equipment categories like dryers, ovens, and microwave systems, then customizes specific aspects such as capacity, materials of construction, automation level, and process-specific features around that proven base rather than designing every project entirely from a blank sheet. This approach captures much of the cost and lead-time benefit of standardization for the well-understood aspects of equipment design while still delivering genuine customization where the client's process actually requires it. Fully custom engineering is reserved for genuinely novel applications where no proven platform exists as a starting point. Clients benefit from understanding which aspects of their requirement are truly unique versus which could use a proven base design, since pursuing full customization on every aspect of a project, even where standardization would work fine, unnecessarily increases both cost and schedule risk.
Kerone designs civil foundations, utility connections, and structural layouts with reserved space and capacity margin for anticipated future expansion phases, even when only the initial phase is being built immediately. Modular equipment architecture, where additional process trains or capacity modules can be added alongside existing equipment, is preferred over monolithic designs that would require complete replacement to expand. Control system architecture is specified with headroom for additional I/O points and equipment integration rather than sized exactly to initial scope. This forward-looking approach requires clients to share their growth projections during the initial design phase, even if uncertain, since incorporating expansion flexibility into the original design is substantially cheaper than retrofitting it later. Projects where future capacity needs were not discussed upfront often face more expensive and disruptive expansion paths than projects where this consideration was built into the original engineering.
Value engineering means systematically reviewing a design to identify where specification requirements exceed what the actual process genuinely needs, then adjusting the design to deliver the required performance at lower cost without compromising functionality, safety, or quality outcomes. Examples include right-sizing equipment capacity to match realistic throughput rather than oversized margins, standardizing on proven component platforms instead of fully custom designs where standardization doesn't compromise process requirements, and optimizing materials of construction to match the actual process chemistry rather than defaulting to premium materials beyond what's needed. Value engineering is most effective when conducted collaboratively between the client's process knowledge and Kerone's equipment design expertise, since cost reduction decisions need to be evaluated against actual process risk rather than made in isolation by either party without full visibility into the tradeoffs involved.
Kerone supports international projects through a combination of remote engineering collaboration during the design phase, factory acceptance testing conducted at Kerone's manufacturing facilities with client representatives able to attend in person or remotely, and on-site installation and commissioning support delivered through Kerone's own teams or regional partner offices across Europe, Southeast Asia, the Middle East, Africa, and the Americas. Equipment is engineered to comply with the destination market's applicable codes and standards, such as CE marking for Europe or specific regional electrical and safety codes, determined during the design phase rather than retrofitted after fabrication. Logistics planning accounts for shipping, customs, and any site-specific installation constraints unique to the destination. Local language and time zone coordination during commissioning is typically handled through Kerone's regional offices or established local partners to ensure responsive support throughout project execution.
An integrated engineering partner like Kerone takes responsibility for how process, mechanical, electrical, and automation elements work together as a single system, whereas sourcing equipment from multiple specialized suppliers requires the client to manage interface compatibility, control system integration, and accountability when something doesn't perform as expected across supplier boundaries. With a single integrated provider, performance guarantees apply to the complete system rather than individual components, and troubleshooting issues that span multiple disciplines, such as a quality problem traced to interaction between heating profile and material handling, is resolved by one team rather than requiring coordination across separate vendors who may each blame the other's equipment. The tradeoff is that an integrated approach may cost more upfront than assembling a system from the cheapest available component suppliers, but it substantially reduces the risk of integration failures and unclear accountability during commissioning and operation.
Let’s Engineer the Right Process.
From application trials to full-scale production systems, our engineering team works with you to develop the right thermal processing solution for your material, throughput, and production requirements.