Continuous Microwave Heating System
Continuous Microwave Heating Systems are industrial-scale processing equipment that apply microwave energy to products moving continuously through the heating zone on conveyors, in tubes, or via pneumatic transport, enabling high-throughput, consistent, and energy-efficient thermal processing without the batch-to-batch variability of discontinuous systems.
Engineered precision for Continuous Microwave Heating System.
Continuous Microwave Heating Systems are industrial-scale processing equipment that apply microwave energy to products moving continuously through the heating zone on conveyors, in tubes, or via pneumatic transport, enabling high-throughput, consistent, and energy-efficient thermal processing without the batch-to-batch variability of discontinuous systems. Products enter the microwave tunnel continuously, receive precisely controlled thermal treatment as they travel through multiple independently controlled microwave zones, and exit in a continuously processed and ready-to-pack or ready-to-use state. Kerone’s continuous microwave heating systems are designed for food processing, chemical production, drying, pasteurization, and industrial material processing applications requiring high throughput, process consistency, and minimal manual intervention.
Our advanced AI, ML, and IoT technologies, this solution delivers smarter automation, real-time insights, and predictive intelligence to enhance efficiency and drive future-ready growth.
Continuous tracking of process parameters with instant adjustments.
Intelligent fault detection to prevent failures before they occur.
Dynamic tuning of operations for maximum output and efficiency.
The thermodynamic architecture of our Continuous Microwave Heating System incorporates advanced thermal modeling and computational fluid dynamics (CFD) to ensure optimal heat and mass transfer across the entire processing zone. By precisely controlling thermal gradients, air velocity profiles, and direct energy delivery mechanisms, the system achieves uniform treatment while preventing localized overheating, product degradation, or thermal stress. This balance of intensive heat transfer and controlled retention time ensures maximum operational throughput with minimal specific energy consumption.
Built with heavy-duty structural engineering and sanitary metallurgy, each unit is manufactured to withstand continuous 24/7 industrial operating conditions. Contact surfaces are finished in high-grade stainless steel (SS 304, SS 316L, or corrosion-resistant alloys) with sanitary mirror-polish options, CIP/SIP washdown provisions, and hermetic chamber sealing. This guarantees full compliance with stringent international hygiene, CE machinery directives, and cGMP standards across food, pharmaceutical, specialty chemical, and heavy manufacturing applications.
Proprietary control algorithms ensure strict process repeatability, while built-in safety interlocks and electromagnetic shielding comply with international CE and OSHA standards. Full process development support — including material loss tangent testing, moisture sorption isotherms, and pilot trials at our Ambernath R&D facility — ensures the selected technology matches your exact industrial throughput goals.
Product & Systems Gallery
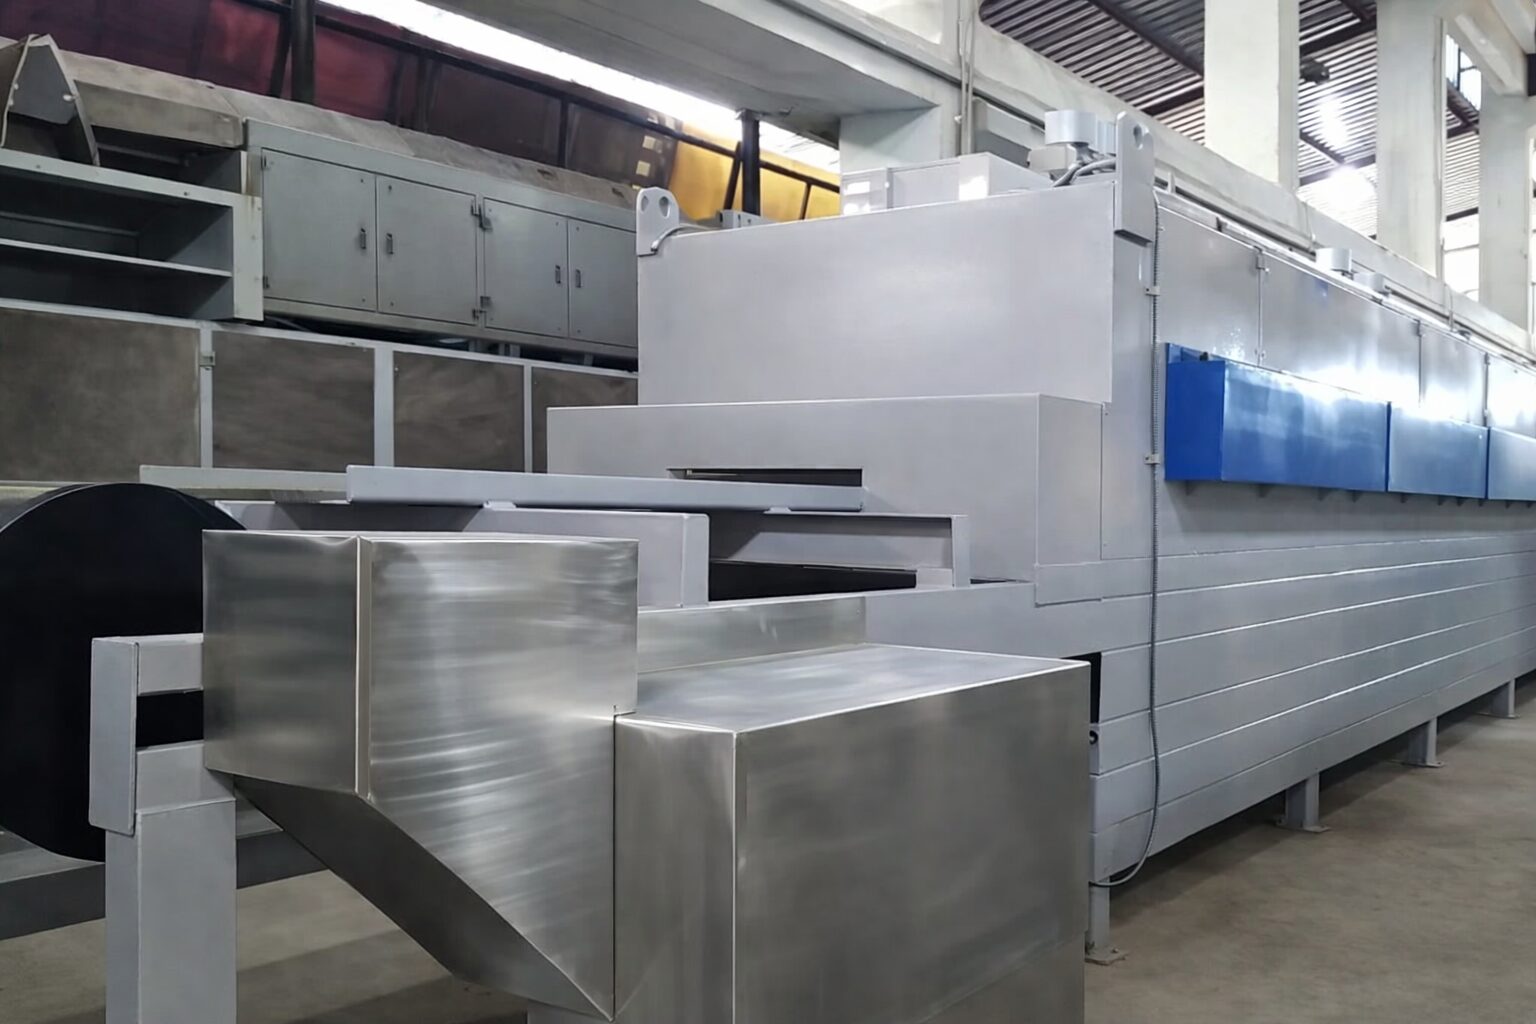
Explore authentic high-resolution photographs of industrial machinery, pilot trial rigs, and continuous turnkey processing installations engineered by Kerone Engineering Solutions for Continuous Microwave Heating System. Each system is fabricated at our ISO 9001:2015 certified manufacturing facilities with precision laser cutting, robotic welding, and stringent Factory Acceptance Testing (FAT).
Continuous Microwave Heating System
Click to view high-res
Continuous Microwave Heating System
Click to view high-res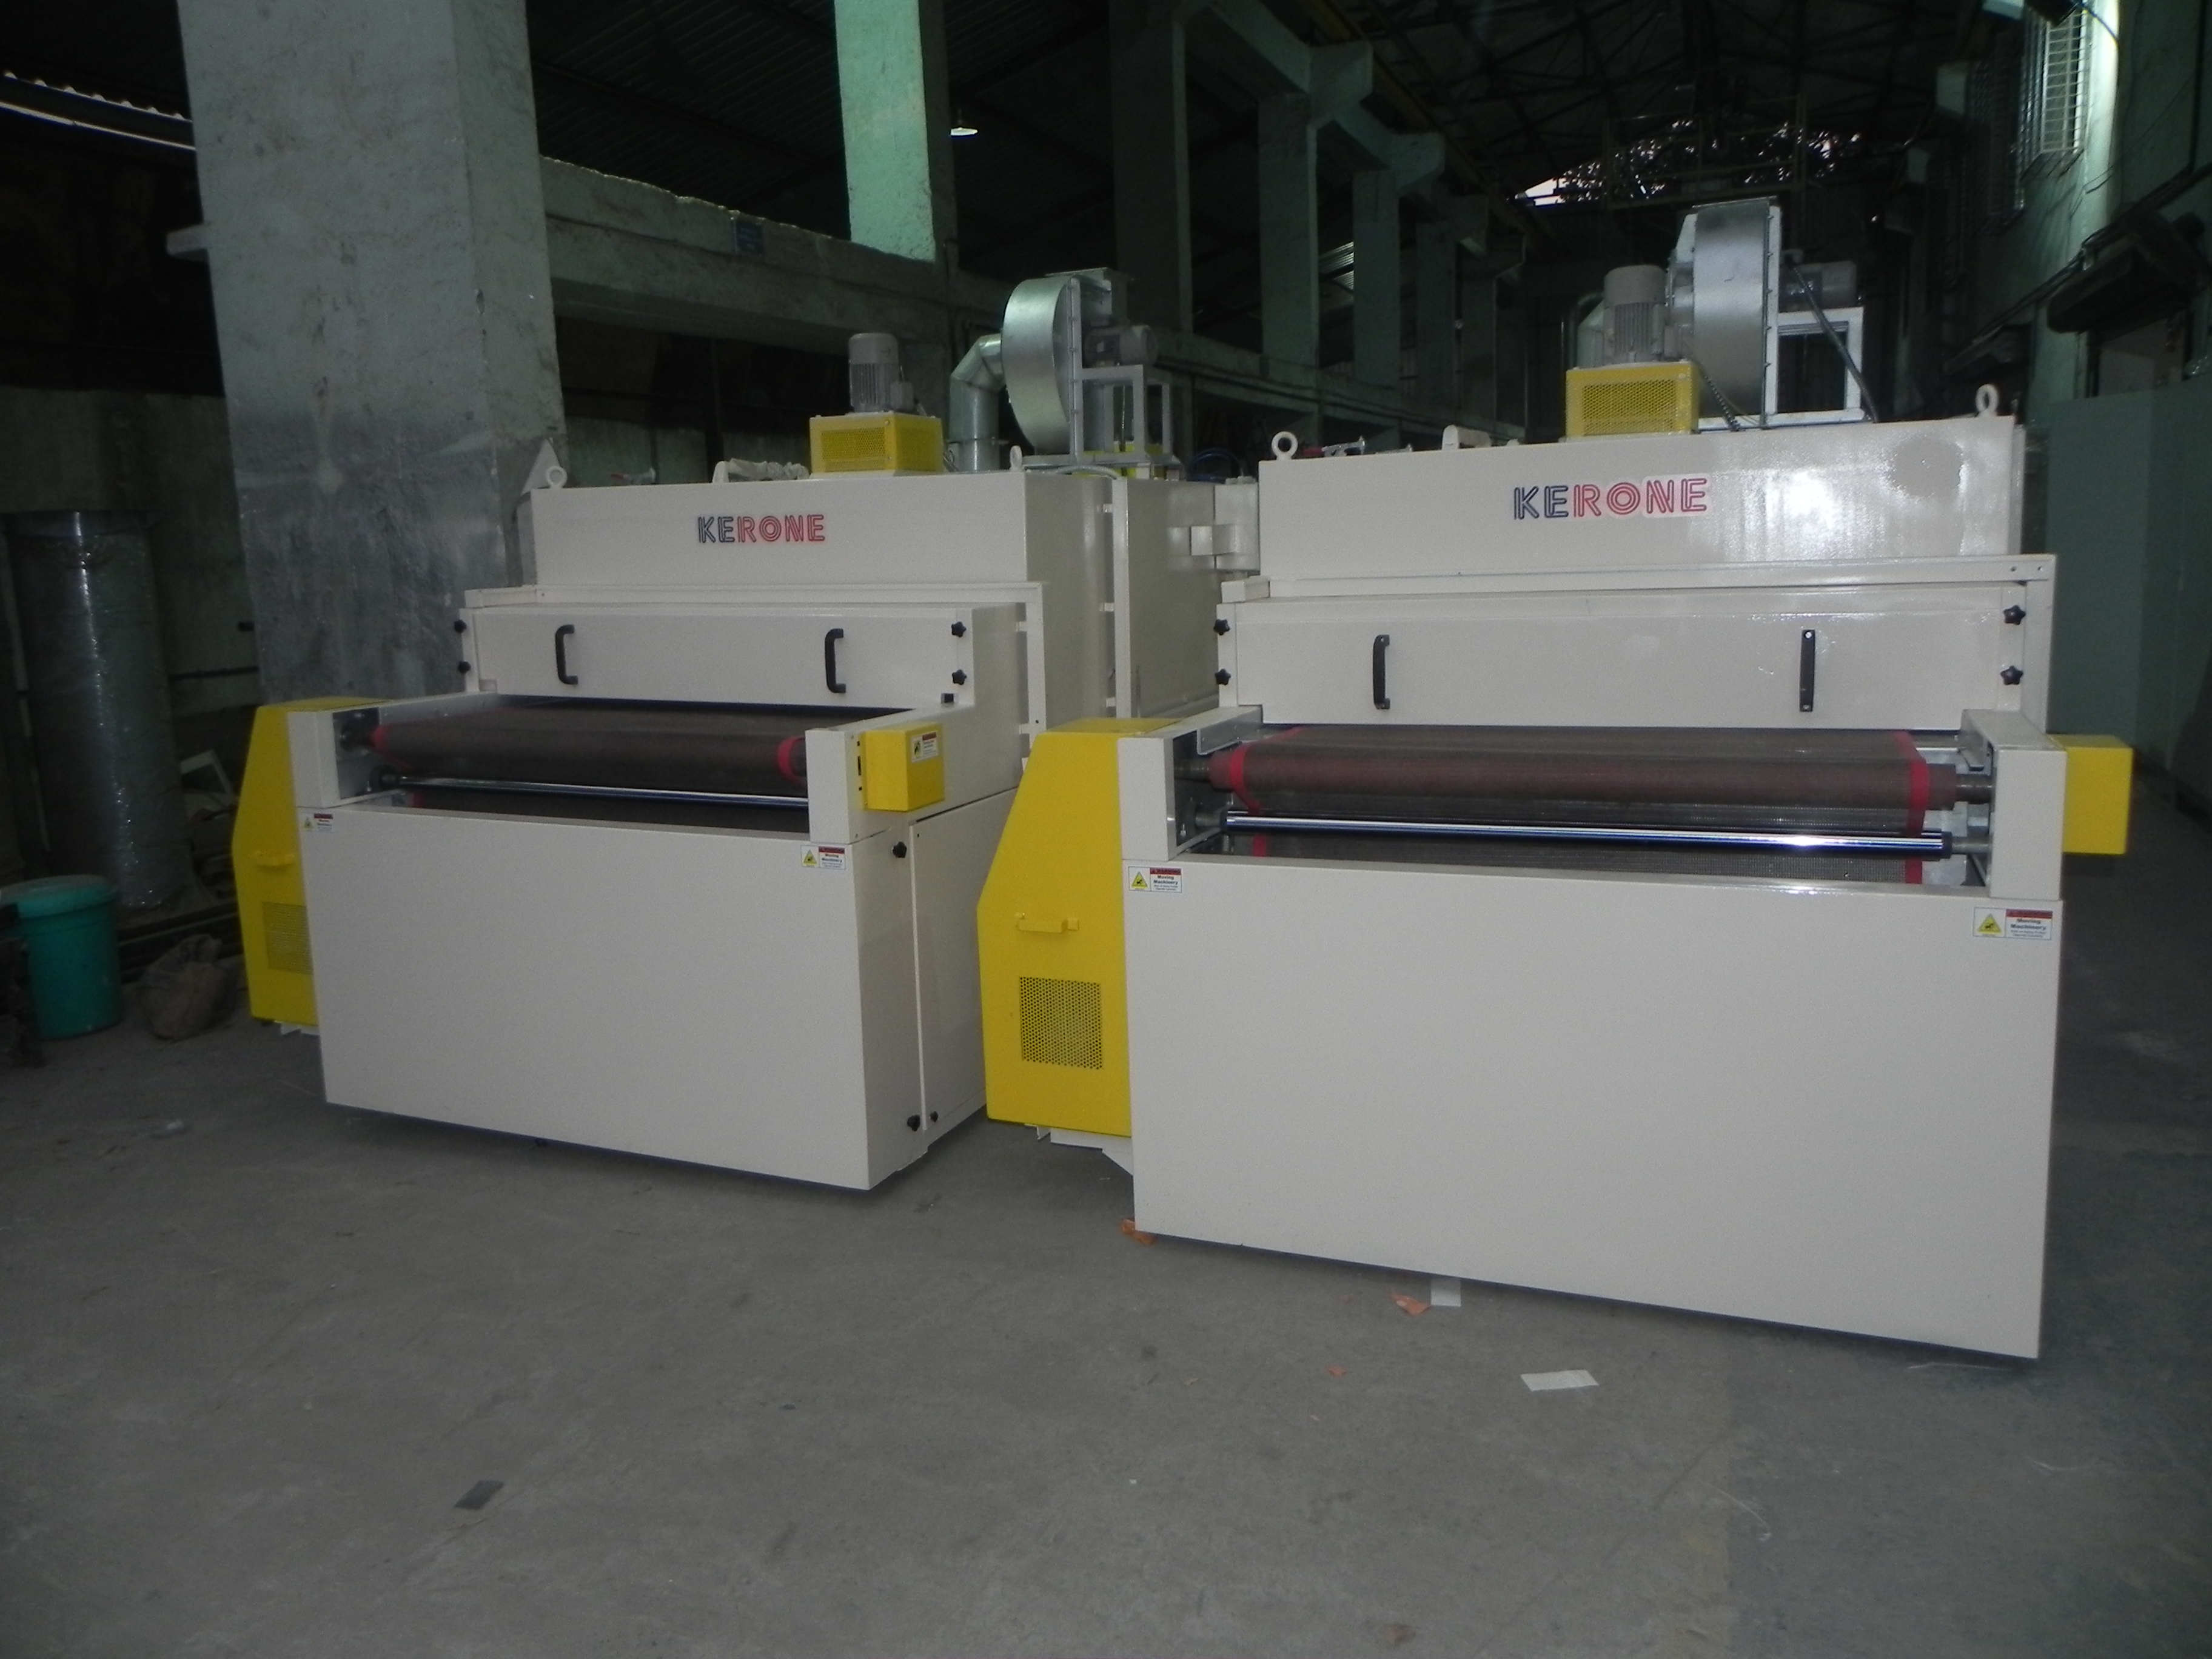
Continuous Microwave Heating System
Click to view high-res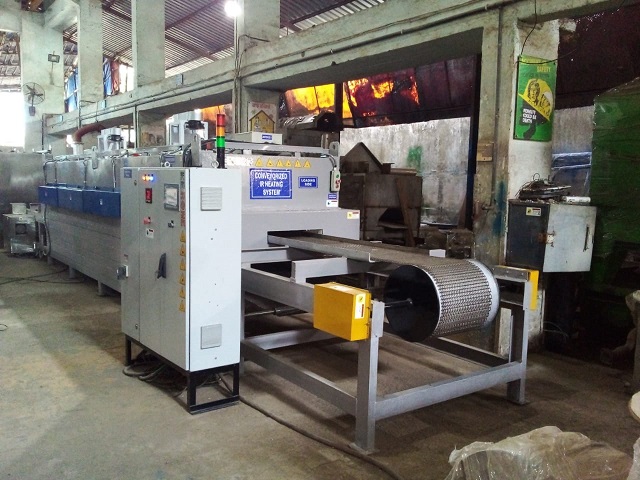
Continuous Microwave Heating System
Click to view high-res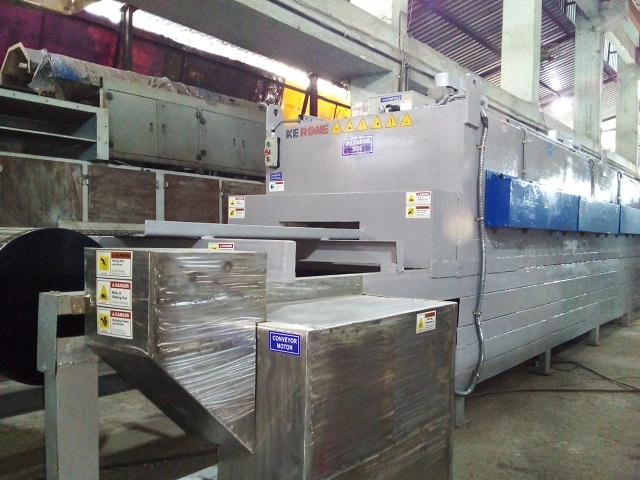
Continuous Microwave Heating System
Click to view high-res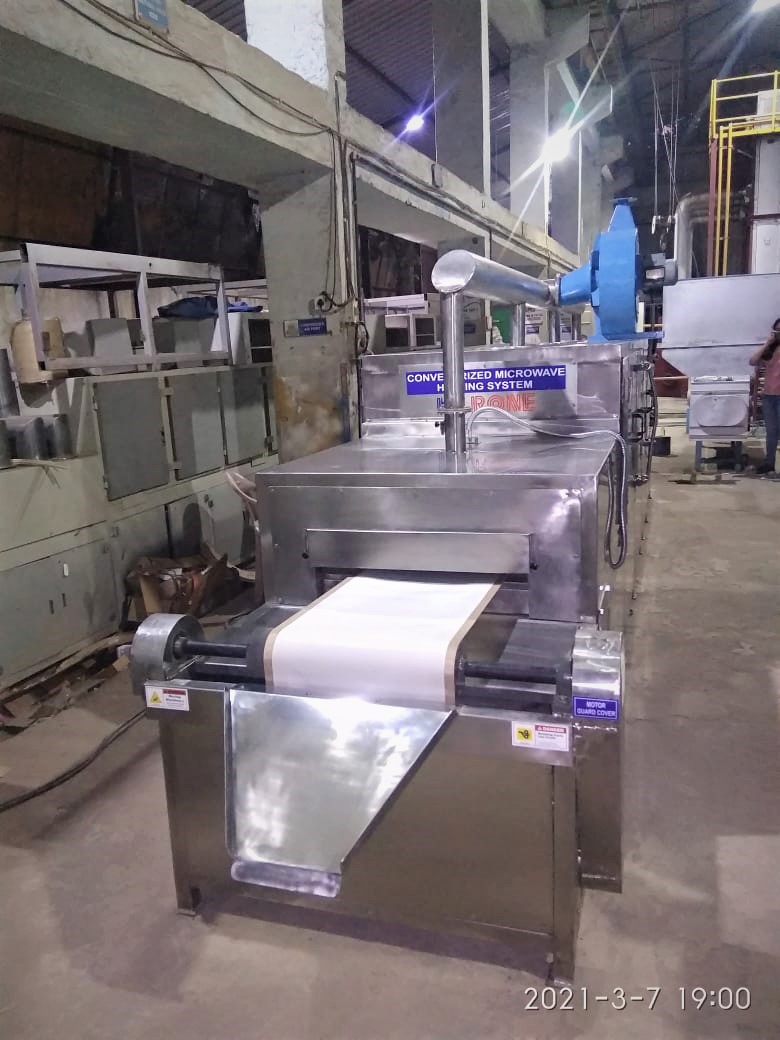
Continuous Microwave Heating System
Click to view high-res
Continuous Microwave Heating System
Click to view high-res
Continuous Microwave Heating System
Click to view high-res
Continuous Microwave Heating System
Click to view high-res50+ Years of Thermal Engineering Leadership.
Since 1976, Kerone Engineering Solutions has delivered over 5,000 custom-engineered thermal and process installations across 50+ countries. In technical collaboration with premier global institutions like CSIR-CEERI and University of Nottingham research partnerships, we design and manufacture high-efficiency machinery that minimizes production downtime and cuts operating expenses.
Unlike standard off-the-shelf equipment suppliers, Kerone operates a complete pilot-scale testing facility at our KRDC Ambernath center. We validate your exact raw material properties — determining moisture sorption isotherms, specific heat capacity, and dielectric behavior — before finalizing equipment sizing, ensuring zero risk during industrial scale-up.
Engineering precision, built into every system.
High Thermal and Processing
High thermal and processing efficiency
Low Maintenance and Easy
Low maintenance and easy operation
Suitable
Suitable for heat-sensitive materials
Fully Adjustable and
Fully adjustable and customizable process parameters
Available in Batch and
Available in batch and continuous configurations
Uniform Processing and
Uniform processing and consistent product quality
Powered by AI, Machine Learning & Smart IoT Integration
Modern industrial processing requires unprecedented thermal precision, energy efficiency, and operational agility. Kerone equips each system with high-speed industrial edge computing controllers, multi-spectral non-contact infrared pyrometry, and proprietary closed-loop machine learning algorithms that continuously analyze process parameters in real time.
The intelligent automation stack monitors dynamic changes in incoming material load, bed thickness, moisture content, and environmental factors. In response, our algorithms dynamically adjust heater power arrays, generator frequency, conveyor drive velocities, and exhaust dampers within milliseconds — entirely eliminating product burn, under-processing, or thermal hotspotting.
Seamlessly integrated with factory-wide SCADA and enterprise ERP architectures via native MQTT, OPC-UA, and Modbus TCP protocols, our systems deliver complete digital recipe control, remote diagnostics, predictive maintenance alerting, and tamper-evident batch logs compliant with global FDA 21 CFR Part 11 and cGMP standards.
Adaptive Heat Modulation
Neural algorithms detect material thermal variations in real time (<50ms response) and tune generator frequency and power arrays automatically.
IoT Cloud Telemetry
Continuous bidirectional telemetry stream via MQTT/OPC-UA protocols directly to centralized plant SCADA, MES, or mobile engineer dashboards.
Predictive Maintenance
Monitors magnetron cathode current, vibration frequency signatures, and differential filter pressure to schedule AMC maintenance before failures occur.
Quality & Batch Traceability
Automated digital recipe execution, multi-stage temperature ramp/soak curves, and cryptographically signed electronic batch logs compliant with 21 CFR Part 11.
Engineered for High-Value Industrial Sectors
Tailored thermal and process configurations across continuous manufacturing lines.
Continuous drying of snacks, pasta,...
Continuous drying of snacks, pasta, grain, and bakery products
Pasteurization of packaged food pro...
Pasteurization of packaged food products inline with filling and sealing lines
Continuous heating and tempering of...
Continuous heating and tempering of chocolate, fats, and confectionery
Industrial chemical and mineral dry...
Industrial chemical and mineral drying and calcination processes
Rubber and polymer continuous heati...
Rubber and polymer continuous heating and curing applications
Agricultural product drying includi...
Agricultural product drying including grains, seeds, and pulses
Configured to Your Process Window
Technical parameter envelopes across industrial manufacturing and engineering architectures.
Frequently Asked Questions
Engineering answers regarding equipment sizing, integration, and process performance.
Food, chemical, pharma, biomass, rubber, textile and more.
Continuous processing eliminates loading and unloading time, provides consistent product treatment, integrates directly with production lines, and achieves higher throughput with fewer personnel.
Solid pieces, granules, powders, pastes, liquids in containers, and packaged products can be handled in continuous microwave systems with appropriate conveyor or flow design.
Kerone's continuous systems can handle throughput from tens of kg per hour for specialty products to many tonnes per hour for high-volume industrial applications.
Microwave choke structures are designed at the product entry and exit openings to suppress microwave propagation along the product path, ensuring safe operation without physical barriers.
Continuous microwave drying systems use conveyor or tunnel configurations to process materials at high throughput rates, making them suitable for industrial-scale production. Kerone's continuous microwave dryers feature modular design for scalability, stainless steel construction, adjustable belt speeds, integrated moisture sensors with feedback control, and energy-efficient magnetron configurations. They are used in food processing, ceramics, pharmaceuticals, chemicals, and wood products. Continuous systems are significantly more productive and energy-efficient than batch microwave systems for large-scale applications.
Continuous microwave tunnels typically divide the treatment path into multiple independently controlled zones, each with its own power setting, rather than applying a single uniform power level along the entire tunnel length. This zoning allows higher power early in the tunnel where bulk heating is needed, tapering to lower power in later zones for fine temperature control as the product approaches target temperature, which avoids overheating the product's leading edge while still achieving adequate treatment by the time it exits. Without independent zone control, operators would need to compromise between underheating the product exit point and overheating the entry point, since a single power setting can rarely satisfy both requirements simultaneously across products with any meaningful residence time in the tunnel.
Throughput is fundamentally a function of conveyor speed and the cross-sectional loading of product on the belt, but the tunnel length and number of zones constrain how much total energy can be delivered within the available residence time at a given speed. Increasing conveyor speed to raise throughput reduces residence time per unit of product, which must be compensated for by either increasing total power or extending tunnel length to maintain the same total energy delivery; simply speeding up the belt without one of these adjustments under-treats the product. This is why tunnel lengths from 2 meters to over 20 meters are offered across different system models, since the required combination of speed, power, and length depends on the specific product's mass, moisture content, and target temperature rise.
Pneumatic transport moves product through the microwave treatment zone suspended in an air or gas stream within enclosed tubing, which works well for free-flowing powders and small granules where even, all-around microwave exposure is desirable and where a solid conveyor belt would create uneven heating on the product's underside facing the belt. Belt conveyor systems instead move product on a stationary support surface through the microwave zone, which suits larger or irregularly shaped items, packaged products, or materials prone to settling or clumping if pneumatically conveyed. Pneumatic systems also tend to achieve more uniform particle-to-particle heating for fine powders since each particle is more individually exposed, while belt systems can experience some shadowing effect in densely packed product layers.
Uneven width-wise heating typically results from standing wave patterns within the microwave cavity creating zones of higher and lower field intensity, or from uneven product distribution across the belt width causing thicker sections to underheat relative to thinner sections. Mode stirrers or rotating elements within the cavity help disrupt standing wave patterns to even out field distribution, while multiple smaller magnetrons distributed across the tunnel width rather than a single large source also improve uniformity compared with single-source designs. On the product side, ensuring consistent layer thickness and even distribution across the belt width through proper infeed design addresses the product-side contribution to uneven heating, which is just as often the root cause as the microwave field distribution itself.
Microwave choking refers to specialized waveguide structures positioned at the openings where product enters and exits the microwave cavity, designed to suppress microwave energy propagation along the product path beyond the treatment zone while still allowing the physical product to pass through freely. Without effective choking, microwave energy could leak out through these openings, creating both a safety hazard for nearby personnel and an efficiency loss as energy escapes rather than being absorbed by the product. Choke design needs to account for the specific opening size and shape required by the product being processed, since a choke effective for thin sheet products may not provide adequate suppression for a larger opening needed to accommodate bulkier items.
Uniform products like grains or pellets heat relatively predictably since their consistent size and shape allow process parameters to be validated once and applied reliably across the full batch. Irregularly shaped or variably sized products, such as mixed vegetable pieces or non-uniform meat cuts, present more of a challenge because thinner sections heat faster than thicker sections under the same microwave exposure, risking either underheated thick spots or overheated thin spots if treated uniformly. Processing variable-shape products successfully often requires either pre-sorting to reduce size variation, accepting a wider target temperature tolerance band, or combining microwave with a finishing step using another heating method to even out any temperature differential remaining after the microwave stage.
Increasing throughput by raising conveyor speed while holding power constant reduces the energy delivered per unit of product, which works only if the product requires less total energy than originally budgeted, otherwise the product simply exits under-treated. Increasing power while holding speed constant raises energy delivery per unit but also raises peak instantaneous power density, which can increase the risk of localized overheating or scorching in sensitive products even though average treatment improves. The more sustainable path to higher throughput is usually extending tunnel length or adding zones to maintain adequate residence time at higher speed, rather than relying solely on either speed or power adjustments independently, since both have practical ceilings before quality degrades.
Continuous microwave systems are typically designed with standard infeed and outfeed conveyor interfaces matching common industrial conveyor heights and speeds, allowing them to be inserted into an existing production line between, for example, a washing or sizing stage upstream and a packaging or cooling stage downstream. Control system integration usually involves the microwave system's PLC communicating production rate and status signals with the broader line's master control system, so the microwave stage can automatically adjust or pause in coordination with upstream feed rate changes rather than operating as an isolated island within the line. Successful integration depends on confirming conveyor speed compatibility and control signal protocols during the design phase rather than discovering mismatches during installation.
Microwave heating effectiveness depends heavily on a material's dielectric properties, particularly its loss factor, which determines how readily it converts absorbed microwave energy into heat; materials with higher moisture content generally couple with microwave energy more effectively than very dry materials, since water is a strong microwave absorber. Materials with very low moisture content or low dielectric loss factor may heat slowly or unevenly under microwave exposure alone, making them less suited to microwave-only processing without a complementary heating method. Suppliers typically test a representative sample of the specific material in question rather than relying on generic dielectric data for a broad material category, since composition variations within the same general material type can meaningfully affect microwave absorption behavior.

Let’s Engineer the Right Process.
From application trials to full-scale production systems, our engineering team works with you to develop the right thermal processing solution for your material, throughput, and production requirements.